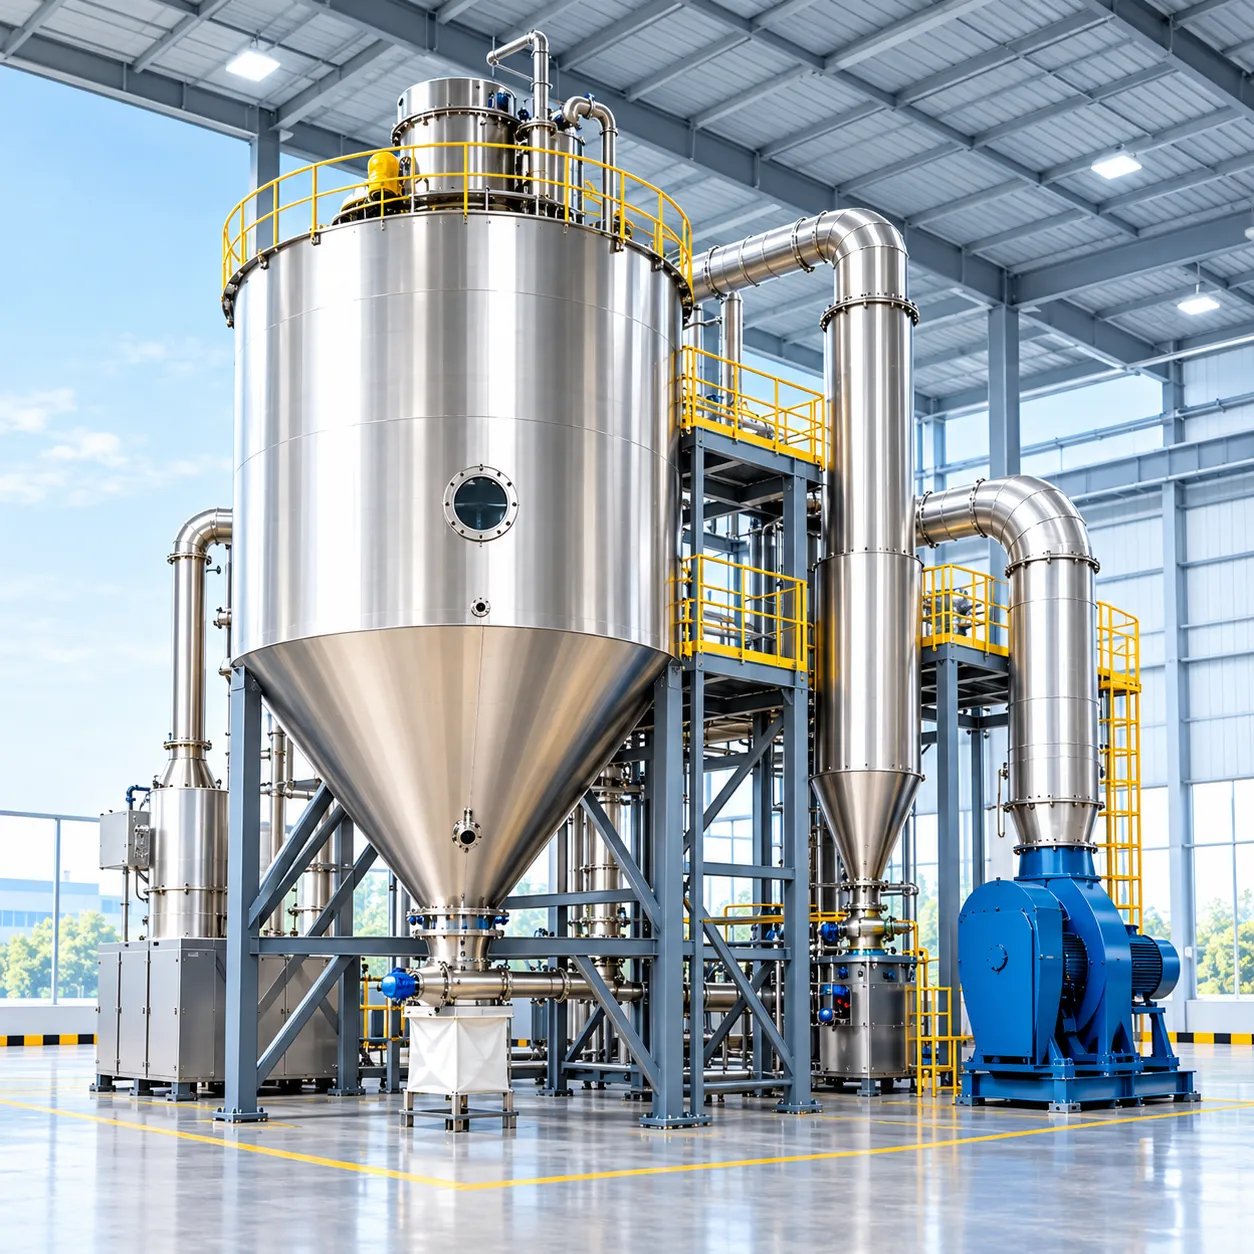

Every kilogram of water an evaporator removes must absorb a large amount of latent heat, and in most plants that heat comes from boiler steam. For dairies concentrating whey, chemical units thickening process streams and factories reducing effluent for zero liquid discharge, steam is often the biggest recurring utility cost after raw materials. Traditional answers such as adding more effects help, but there is a limit to how far they can go.
Mechanical vapor recompression (MVR) takes a different route. Instead of sending vapor to a condenser or to the next effect, it compresses the vapor and sends it straight back to heat the same evaporator. Once the plant is running, it needs very little live steam, and its main energy input becomes electricity. This article explains how MVR works, why it saves so much steam, where it fits best and what to check before investing in one.
The Problem MVR Solves
When water boils in an evaporator, the vapor it produces carries almost all the latent heat that was put in. In a single effect evaporator, that heat is dumped into cooling water. In a multiple effect evaporator, the vapor is reused a few times before it reaches the condenser, which raises steam economy to around 2.5 for a triple effect plant and higher for more effects. Even so, a meaningful share of energy is still discarded at the final condenser, and each extra effect adds equipment cost while saving progressively less steam.
The vapor leaving an evaporator is too cool to heat the liquid that produced it, because heat only flows from a hotter body to a cooler one. MVR solves that by adding a small amount of mechanical energy to raise the vapor's pressure and therefore its condensing temperature. The upgraded vapor is now a few degrees hotter than the boiling liquid and can serve as the heating medium again.
How an MVR Evaporator Works
The cycle can be described in a few steps:
- Start-up: Live steam is used briefly to bring the evaporator and liquid up to operating temperature and generate the first vapor.
- Evaporation: Feed liquid is distributed over the heat transfer surface, usually as a falling film inside vertical tubes, where it boils and releases vapor.
- Separation: The vapor-liquid mixture enters a separator. Concentrate is recirculated or withdrawn, while clean vapor flows to the compressor.
- Compression: An electrically driven fan or compressor raises the vapor's pressure and saturation temperature by a few degrees.
- Desuperheating: Compression also superheats the vapor, so a small amount of condensate is often injected to bring it back toward saturation and improve heat transfer.
- Condensation: The compressed vapor enters the shell side of the evaporator, condenses on the tubes and gives up its latent heat to the boiling liquid.
- Heat recovery: Hot condensate and concentrate pass through plate heat exchangers to preheat incoming feed before leaving the system.
During steady operation, a small amount of make-up steam may still be needed to cover heat losses and balance the system, but this is a fraction of what a conventional plant would use.
Types of Compressors Used
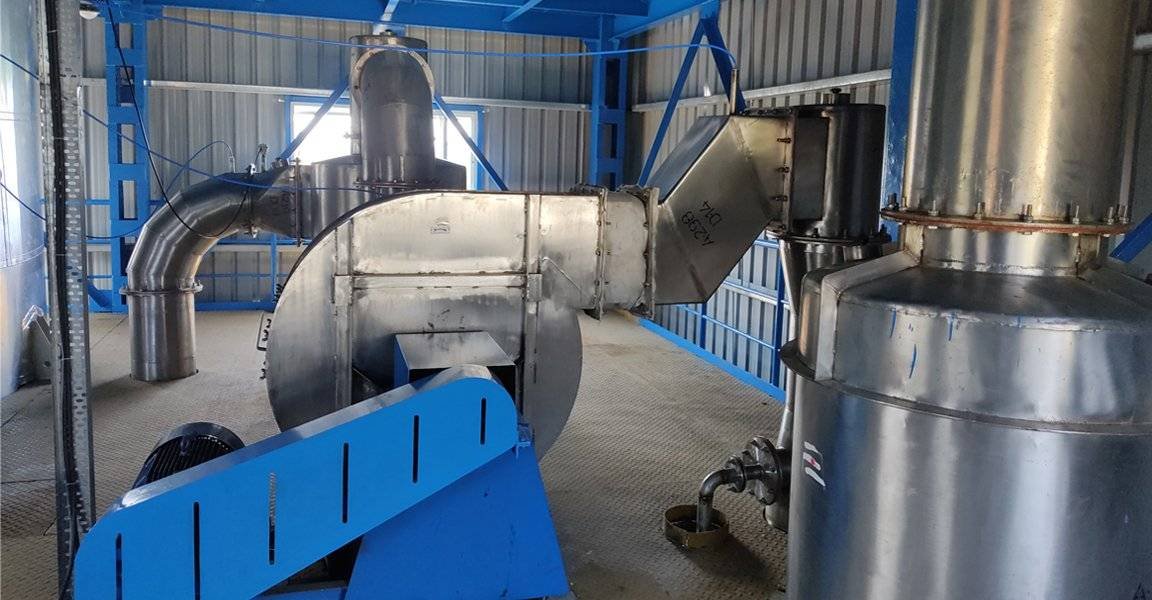
- High-speed turbo fans: Robust, efficient machines that typically provide a modest temperature lift per stage. Several fans can be placed in series when more lift is needed.
- Centrifugal compressors: Provide a larger pressure ratio in a single machine and suit larger plants or liquids that need more temperature lift.
- Positive displacement blowers: Sometimes used in smaller units, though they are less common in large continuous plants.
Why MVR Cuts Steam Costs So Dramatically
The key is the difference between the energy needed to boil water and the energy needed to compress vapor slightly. Boiling a kilogram of water needs roughly 2,200 to 2,400 kJ of latent heat. Raising the pressure of that same kilogram of vapor by a small margin needs only a small fraction of that energy. The compressor recycles the latent heat rather than replacing it.
An Illustrative Example
Consider a plant that must evaporate 10,000 kg of water per hour. The figures below are illustrative only and use typical, hedged values.
- Latent heat load: 10,000 kg/hr x about 2,300 kJ/kg = 23,000,000 kJ/hr, or roughly 6,389 kW of thermal duty.
- Single effect evaporator: At a steam economy of about 0.9, live steam demand is about 11,111 kg/hr.
- Triple effect evaporator: At a steam economy of about 2.6, live steam demand is about 3,846 kg/hr.
- MVR evaporator: Many falling film MVR plants on clean, low boiling point elevation liquids report specific power use often in the range of roughly 10 to 30 kWh per tonne of water evaporated. At 20 kWh per tonne, the compressor would draw about 10 x 20 = 200 kW, plus a small amount of make-up steam.
In this example, the MVR's electrical input is only around 3 percent of the thermal duty it delivers. Electricity is a more expensive form of energy than steam, so the comparison has to be made in money and in emissions, not only in kilowatts. Even so, the result is often a large reduction in total evaporation energy cost. AKSH's evaporator product information notes that continuous MVR plants can lower steam utility expenses by up to 80 to 90 percent compared with conventional systems, though actual savings always depend on the liquid, the design and local utility prices.
Equivalent Steam Economy
Engineers sometimes describe MVR performance as an equivalent number of effects. Because so little live steam is needed per kilogram of water evaporated, an MVR plant can behave like an evaporator with many more effects than would ever be practical to build. That is the main reason MVR is often the first choice for large, continuous duties where steam is expensive.
Where MVR Delivers the Best Results
MVR is not a universal answer. It performs best when several conditions are met together:
- Continuous, steady operation: The compressor investment pays back over many running hours. Plants that operate around the clock benefit most.
- Low to moderate boiling point elevation: Dissolved solids raise the liquid's boiling point. The compressor must provide enough lift to overcome that elevation plus the temperature difference needed for heat transfer, and high elevations increase power demand sharply.
- Favorable power-to-steam cost ratio: Where electricity is reasonably priced relative to steam, MVR economics are strong.
- Clean vapor: Vapor carrying droplets, solids or corrosive components can damage the compressor, so good separation is essential.
- Large evaporation loads: The fixed cost of the compressor and controls is easier to justify at higher capacities.
Typical Applications
- Dairy: Milk, skim milk and whey concentration ahead of spray drying.
- Food and starch: Glucose, starch process water, juices and extracts.
- Chemicals: Salt solutions, caustic, sulfate streams and process mother liquors.
- Effluent treatment and ZLD: Concentrating RO reject and high-TDS wastewater ahead of crystallizers or dryers.
- Pharmaceuticals: Large-volume aqueous streams and solvent-free process water recovery.
MVR vs MEE vs TVR at a Glance
| Factor | Multiple Effect (MEE) | Thermal Vapor Recompression (TVR) | Mechanical Vapor Recompression (MVR) |
|---|---|---|---|
| Main energy input | Live steam to first effect | High-pressure motive steam | Electricity, plus small make-up steam |
| Live steam use | Moderate, falls with more effects | Lower than equivalent MEE | Very low once running |
| Cooling water use | Moderate | Moderate | Very low |
| Capital cost | Moderate to high | Low addition to an MEE | Higher, due to compressor |
| Moving parts in vapor path | None | None | Rotating compressor or fan |
| High boiling point elevation | Handles well | Handles moderately | Can be limiting |
| Best fit | Where steam is cheap or liquid is difficult | Upgrading existing falling film plants | Large continuous duties with reasonable power cost |
Hybrid systems are common. A plant may use MVR for bulk evaporation of a clean, dilute stream and a small steam-heated forced circulation finisher for the final, high-concentration stage where boiling point elevation and scaling become severe.
Design Considerations for an MVR Plant
Evaporator Type
Because the compressor can only provide a limited temperature lift, the evaporator must work on a small temperature difference. Falling film tubes are the usual choice for this reason, as explained in our comparison of falling film and rising film evaporators. For scaling or crystallizing liquids, forced circulation MVR designs are used instead.
Heat Transfer Area
A small temperature difference means a larger heat transfer area for the same duty. Designers balance compressor power against area: a little more lift reduces the area needed but raises power demand. The trade-off starts with an accurate mass and energy balance, which our evaporator capacity calculation guide covers in detail.
Fouling Management
With a small driving temperature difference, any fouling layer has an outsized effect, because it consumes a bigger share of the available lift. Feed pretreatment, correct wetting rates, controlled velocities and a planned cleaning schedule are therefore critical. See our guide to preventing evaporator fouling for practical measures.
Materials of Construction
Effluent and chemical streams can be corrosive, especially when chlorides are concentrated. Material selection for tubes, separators and compressor wetted parts must reflect the actual liquid chemistry. AKSH's industrial evaporators are built in SS304, SS316 and SS316L, as well as duplex steel, titanium and Hastelloy where the duty demands it.
Controls and Protection
An MVR plant is a tightly coupled system. Compressor speed, vapor pressure, make-up steam, feed rate, recirculation and concentrate density must be controlled together, and the compressor needs protection against surge, overspeed and liquid carryover. AKSH's instrumentation, automation and controls packages provide PLC and SCADA control with interlocks, alarms and trend logging, so operators can see how specific energy use changes over time.
Maintenance and Reliability
The compressor is the one major rotating machine in the vapor path, so its upkeep deserves attention from the start. Plan for routine checks of bearings, lubrication, vibration and seals, keep critical spares on site, and monitor the trend of power consumption per tonne of water evaporated. A gradual rise in that figure is often the earliest sign of fouling or a developing mechanical issue.
MVR in Zero Liquid Discharge Systems
Thermal evaporation is usually the most energy-intensive part of a ZLD scheme. After RO has recovered as much water as membranes can, the reject brine must be concentrated thermally before crystallization or drying. Using MVR for this stage can significantly reduce the steam load of the whole plant. AKSH's ZLD plants combine pretreatment, high-recovery RO, MEE or MVR evaporation and crystallizers or dryers, with the thermal stage selected according to effluent chemistry and utility costs. For a broader look at the economics, read our cost-benefit comparison of ZLD and conventional effluent treatment.
Is MVR Right for Your Plant? A Quick Checklist
- Does the evaporator run continuously for most of the year?
- Is the evaporation load large enough to justify a compressor?
- Is the boiling point elevation of the liquid low to moderate across the concentration range?
- Is electricity reasonably priced compared with steam at your site?
- Is your boiler capacity constrained, or do you want to reduce boiler fuel and emissions?
- Can the vapor be kept clean enough to protect the compressor?
If most answers are yes, MVR deserves a detailed lifecycle comparison against an MEE or TVR alternative. Evaporation is also only one part of a plant's energy picture; our article on reducing energy costs in industrial processing looks at how evaporation and drying can be optimized together.
Why Choose AKSH Engineering
AKSH Engineering Systems Pvt. Ltd., based in Ahmedabad, Gujarat, has designed and manufactured evaporation, drying and turnkey process plants since 2013, with more than 100 installations. Our team of technocrats brings over 100 years of combined experience. We design and fabricate in-house and size each MVR, MEE or hybrid plant from your real feed data, utility costs and operating pattern. Explore our wider range of sustainability solutions for reducing energy, water and waste across your plant.
Conclusion
MVR evaporators cut steam costs by recycling the latent heat that conventional evaporators discard. A compressor adds a small amount of energy to raise vapor temperature, turning waste vapor into useful heating steam. For large, continuous duties with low to moderate boiling point elevation and sensible power prices, the result is often a dramatic reduction in live steam demand, boiler fuel and cooling water.
Every liquid and every site is different, so the right answer comes from a careful comparison of MVR, MEE, TVR and hybrid options. Share your feed data and utility costs with the AKSH Engineering team, and we will help you evaluate whether MVR is the right investment for your plant.