ZLD Plant
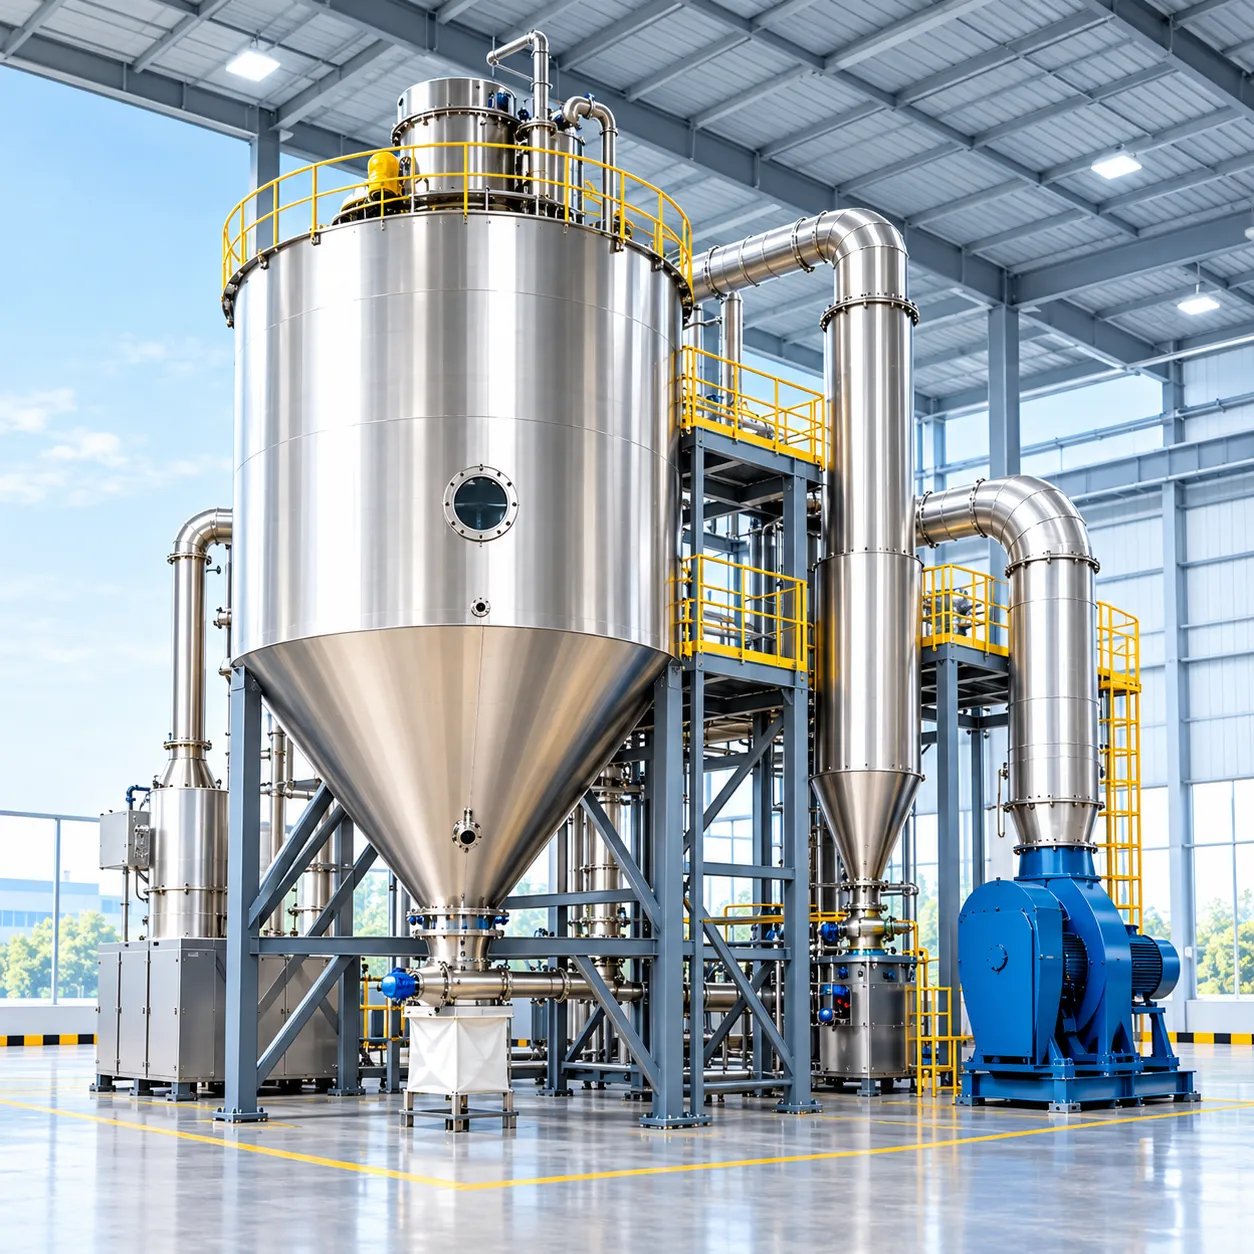
Turnkey Zero Liquid Discharge (ZLD) Plants engineered by AKSH Engineering Systems for complete industrial wastewater recycling and compliance. Combining advanced RO pre-concentration, Multiple Effect Evaporators (MEE/MVR), and Crystallizers to deliver up
Advanced Zero Liquid Discharge (ZLD) Plants & Turnkey Systems
AKSH Engineering Systems Pvt. Ltd. is a leading manufacturer and turnkey provider of high-performance Zero Liquid Discharge (ZLD) Plants in India. Designed to eliminate liquid waste emission, enable total water recovery, and comply with strict environmental regulations, our ZLD systems help industries meet environmental norms while maximizing operational sustainability.
Our custom-built Zero Liquid Discharge solutions recover up to 95–98% of industrial wastewater as high-purity water for process reuse, converting dissolved solids into dry, manageable salt cake for disposal or byproduct recovery.
What is a Zero Liquid Discharge (ZLD) System?
A Zero Liquid Discharge (ZLD) plant is an advanced wastewater treatment process designed to purify and recycle virtually all industrial effluent, leaving zero liquid waste discharged into rivers, municipal sewers, or surrounding soil.
By integrating pre-treatment, membrane separation, thermal evaporation, and crystallization, an AKSH ZLD plant ensures complete water closed-loop recycling for high-TDS (Total Dissolved Solids) and heavy industrial effluent.
Core Components of Our ZLD Systems
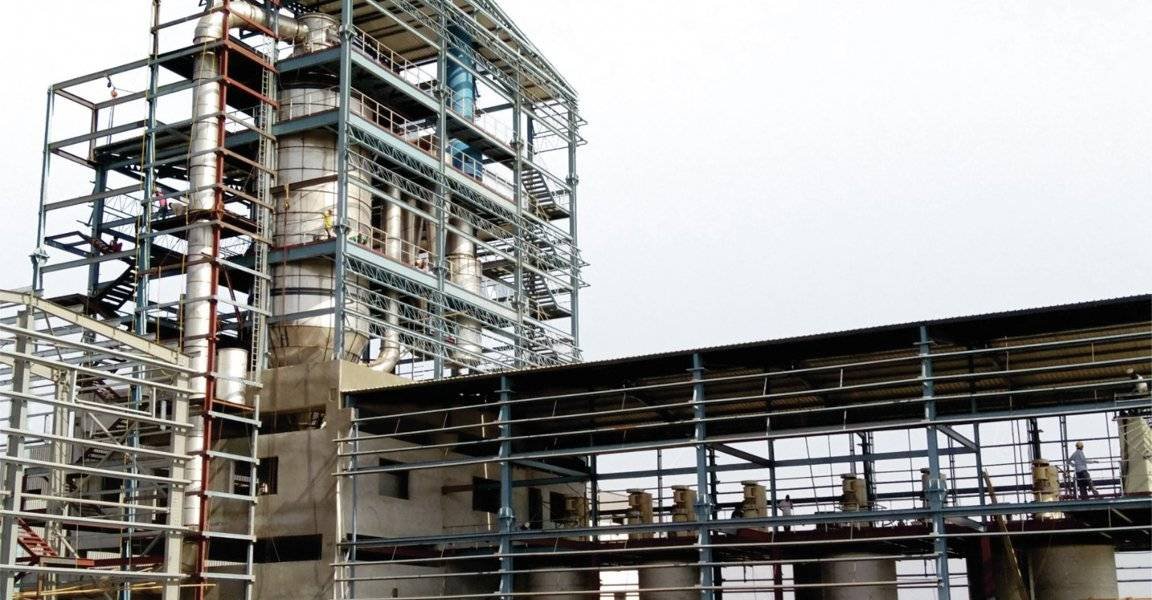
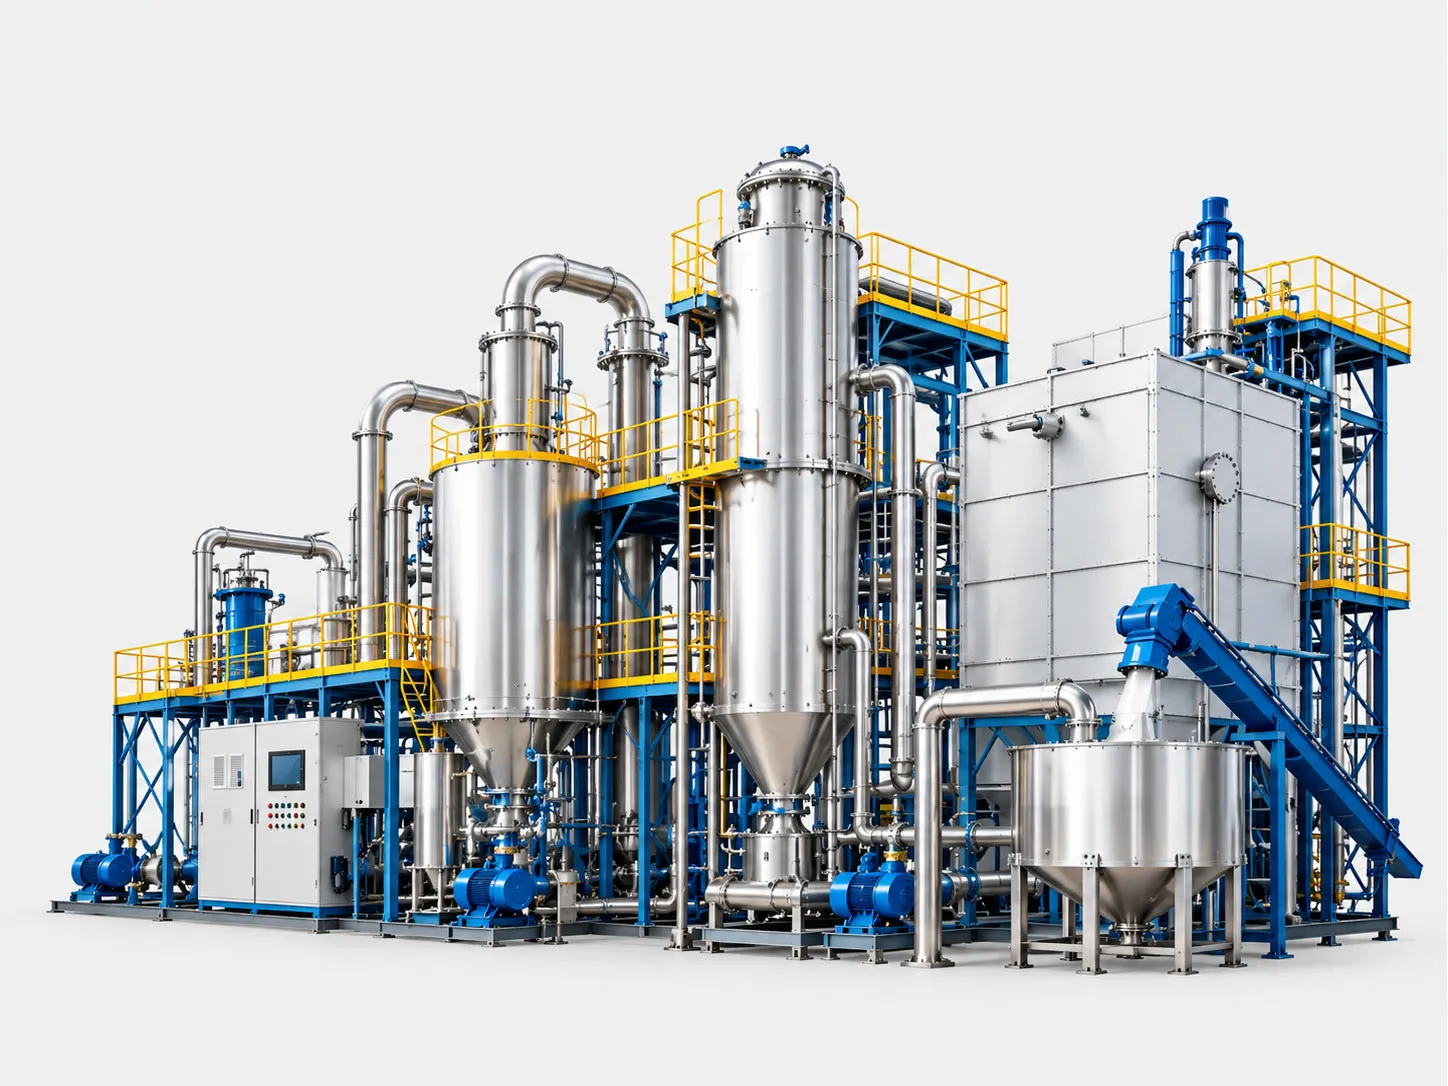
AKSH Engineering designs and fabricates fully integrated, multi-stage ZLD systems configured for optimal lifecycle efficiency:
1. Advanced Pre-Treatment & Filtration
Removes suspended solids, organic loads, heavy metals, and hardness to protect downstream membranes and thermal units from scaling.
-
Technologies: Multi-Grade Filters, Activated Carbon Filters, Ultrafiltration (UF), Softeners, and Chemical Dosing Units.
2. High-Recovery Reverse Osmosis (RO)
Drives initial volume reduction by separating reusable clean permeate water from concentrated brine, reducing overall steam consumption in thermal stages.
-
Features: High-Pressure RO, Disc Tube RO (DTRO), and foul-resistant membrane designs.
3. Thermal Evaporation Unit (MEE / MVR)
Concentrates high-TDS reject brine from the RO stage into a thick, near-saturated slurry.
-
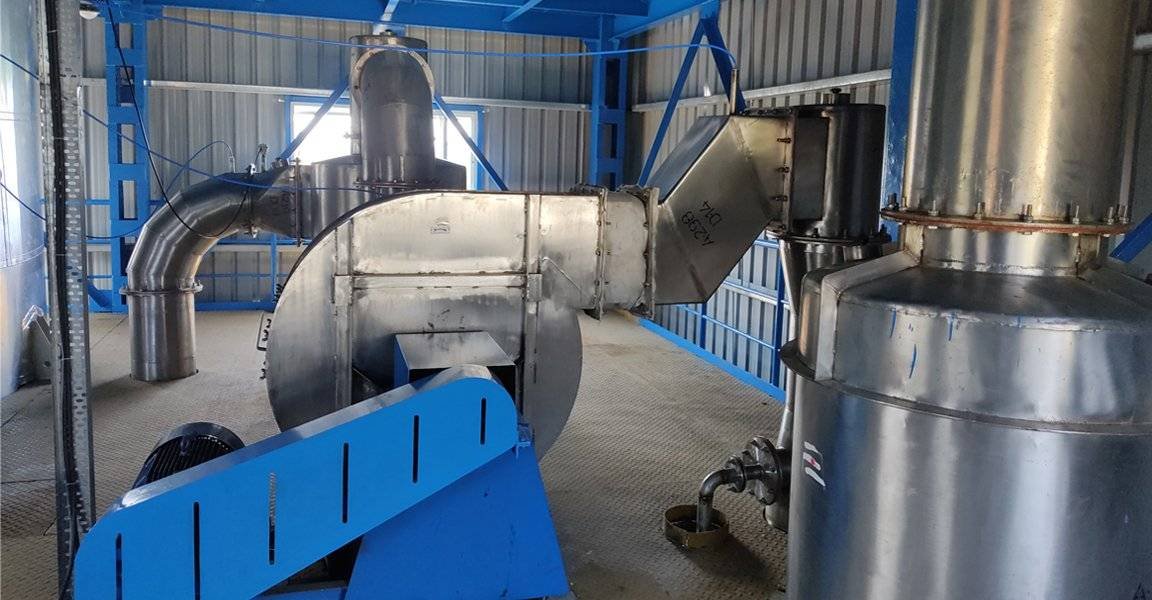
Technologies: Multiple Effect Evaporators (MEE), Mechanical Vapor Recompression (MVR), Forced Circulation Evaporators.
4. Crystallizer & Solids Separation
The final stage that drives remaining moisture out of the concentrated slurry, producing dry salt solids and recovering the final condensate water.
-
Technologies: Forced Circulation Crystallizers, Agitated Thin Film Dryers (ATFD), Centrifuges, and Filter Presses.
Technical Specifications & Capabilities
| Parameter | Specification / Range |
| Plant Capacity | 10 KLD to 5,000+ KLD (Custom Sized) |
| Water Recovery Rate | 95% to 98% Reusable Permeate Water |
| Material of Construction (MOC) | SS316, SS316L, Duplex Stainless Steel, Titanium, Hastelloy |
| Effluent Handling Capabilities | High TDS, High COD/BOD, Scaling Salts, Corrosive Effluents |
| Automation | Fully Automated PLC + SCADA Control with Remote Monitoring |
Why Choose AKSH Engineering ZLD Plants?
-
Optimized Operating Expenses (OPEX): Strategic integration of high-recovery RO with MVR/MEE technology drastically cuts power and steam consumption.
-
Robust Anti-Scaling Design: Engineered flow dynamics and metallurgy prevent fouling in high-salinity thermal and membrane stages.
-
100% Environmental Compliance: Engineered to easily exceed CPCB/SPCB zero-discharge mandates across all state jurisdictions.
-
Turnkey Execution: Complete lifecycle support—from effluent laboratory analysis and process engineering to fabrication, erection, and commissioning.
Key Industries Served
Our ZLD solutions are deployed across diverse water-intensive and regulated industrial sectors:
-
Textiles & Dyeing Units: Color removal, salt recovery, and bulk wash water recycling.
-
Pharmaceuticals & Bulk Drugs: Handling high-COD, high-salinity process effluents.
-
Chemicals & Agrochemicals: Treatment of complex chemical effluent and toxic wastewater streams.
-
Electroplating & Surface Treatment: Metal recovery and acid/alkali wastewater recycling.
-
Distilleries & Power Plants: High-capacity blowdown and spent wash recovery.
Frequently Asked Questions
Have a project in mind?
Talk to our engineers about your drying, evaporation or turnkey process requirement.