Industrial Evaporators
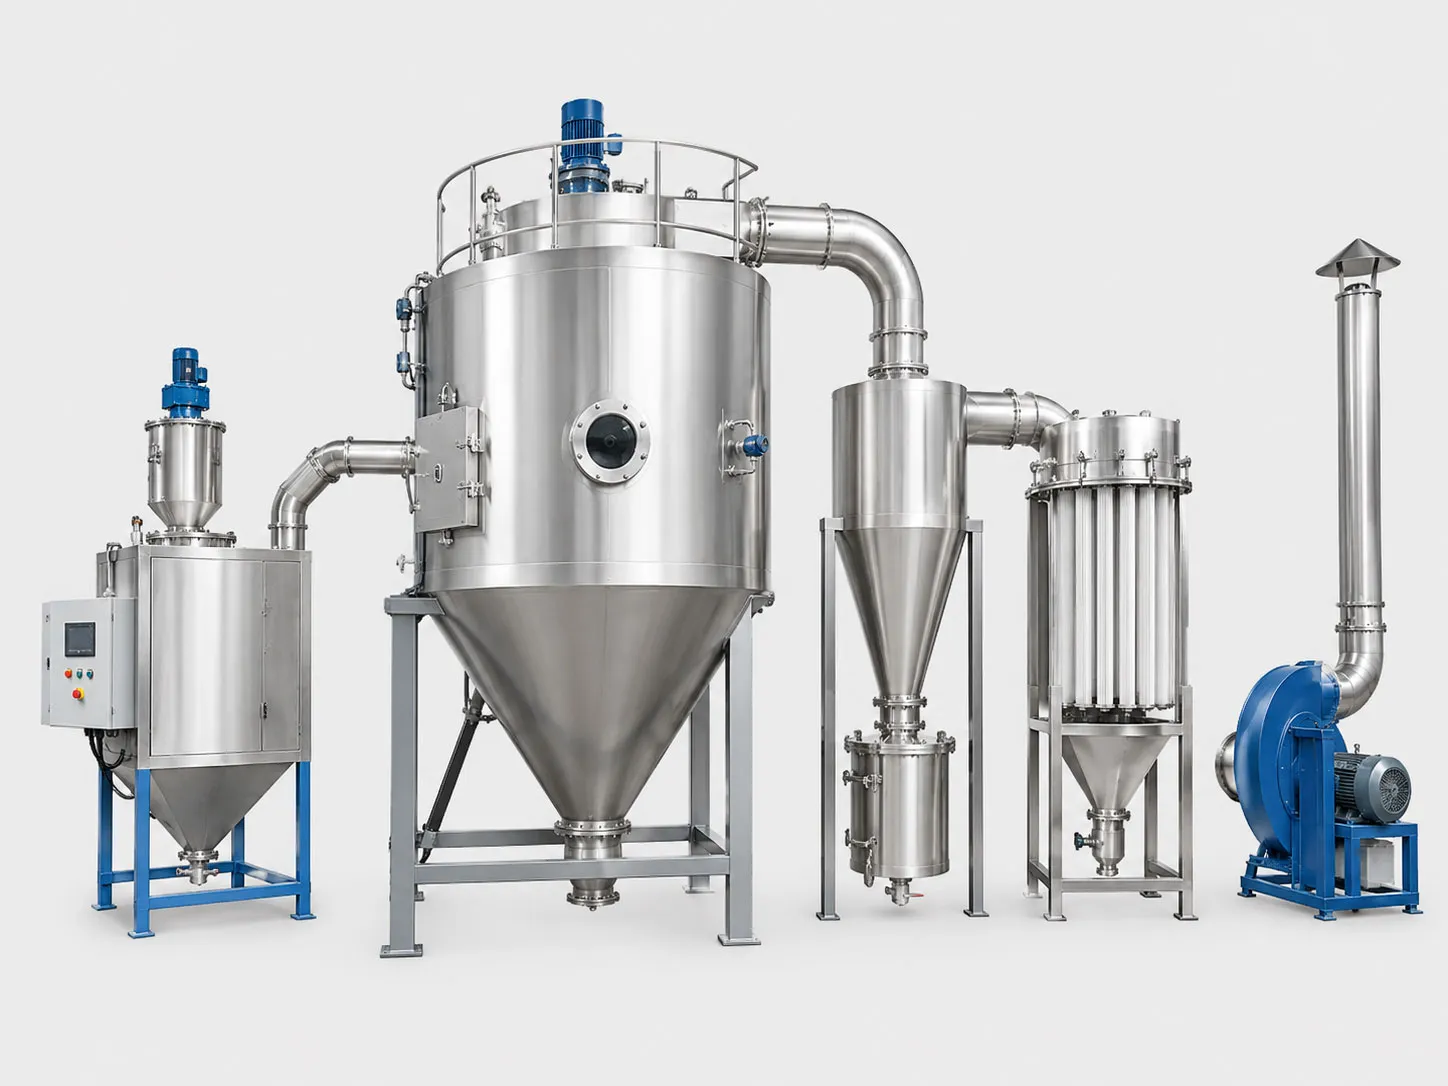
High-performance Industrial Evaporator Plants engineered by AKSH Engineering Systems for optimal concentration, solvent recovery, and Zero Liquid Discharge (ZLD) compliance. Available in Multiple Effect (MEE), MVR, Falling Film, and Forced Circulation con
High-Efficiency Industrial Evaporators & Evaporation Plants
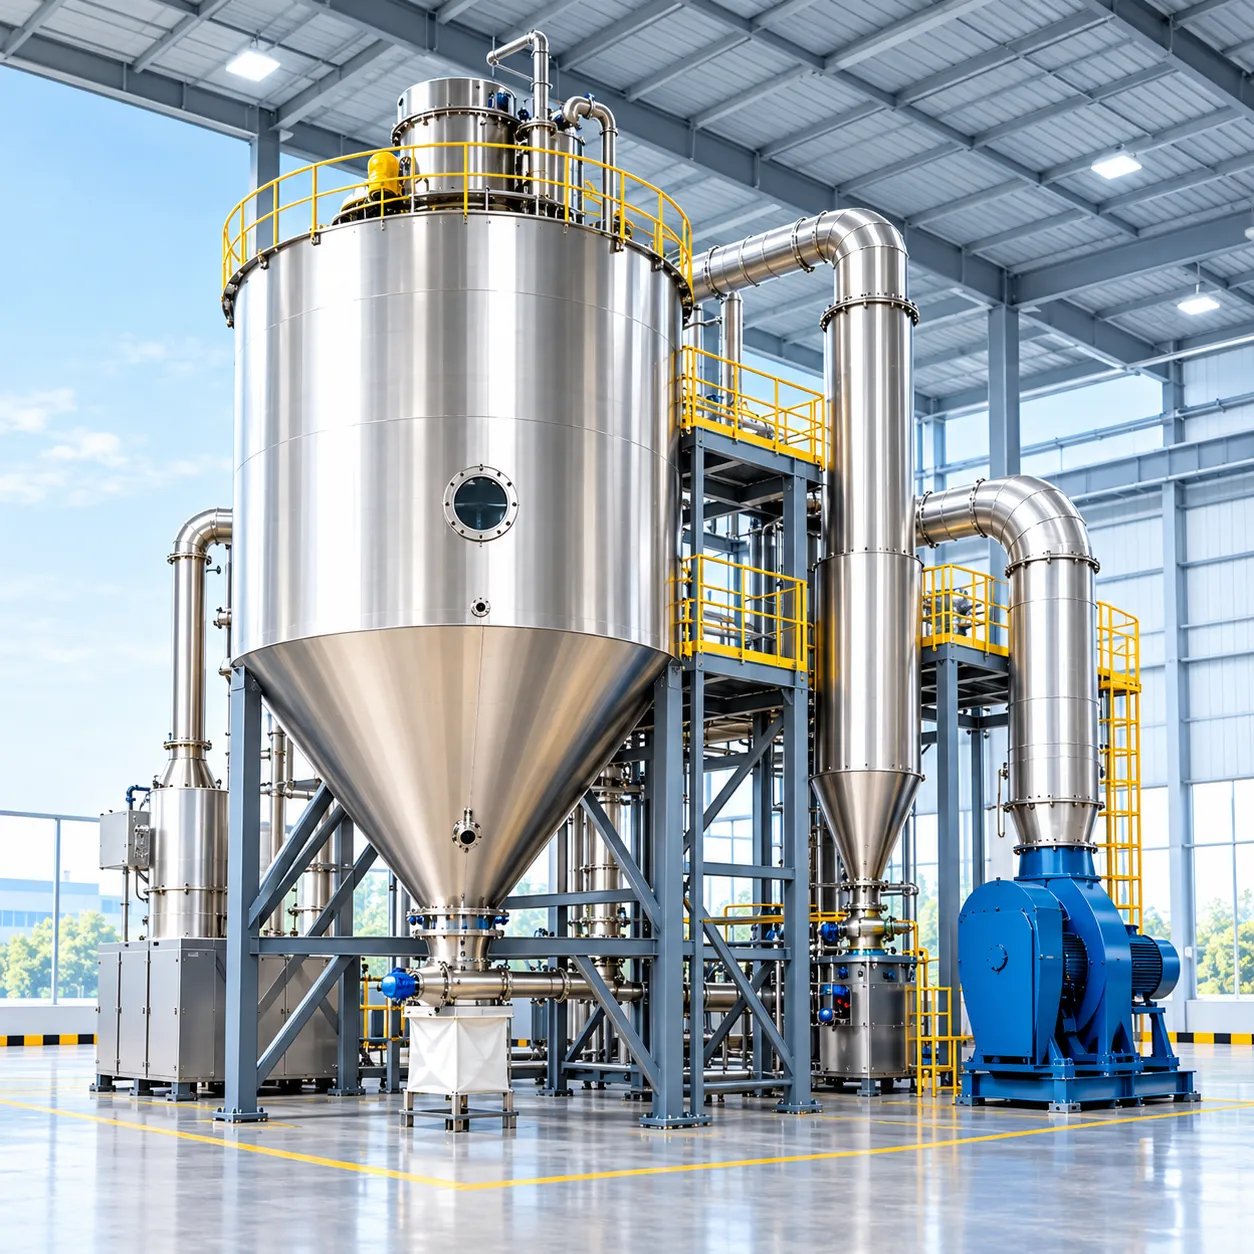
AKSH Engineering Systems Pvt. Ltd. is a premier manufacturer and supplier of high-efficiency Industrial Evaporator Plants based in India. Engineered with advanced thermal designs and energy-recovery mechanisms, our industrial evaporators deliver maximum concentration performance, minimal energy consumption, and high operational reliability across demanding process industries.
Whether you need to recover valuable products, achieve Zero Liquid Discharge (ZLD) compliance, or reduce trade effluent volume, AKSH Engineering provides custom-built evaporation solutions engineered for your specific thermal, chemical, and viscosity parameters.
Our Range of Industrial Evaporation Systems
We design, manufacture, and commission a complete spectrum of industrial evaporation technologies tailored to distinct feed characteristics:
1. Multiple Effect Evaporators (MEE)
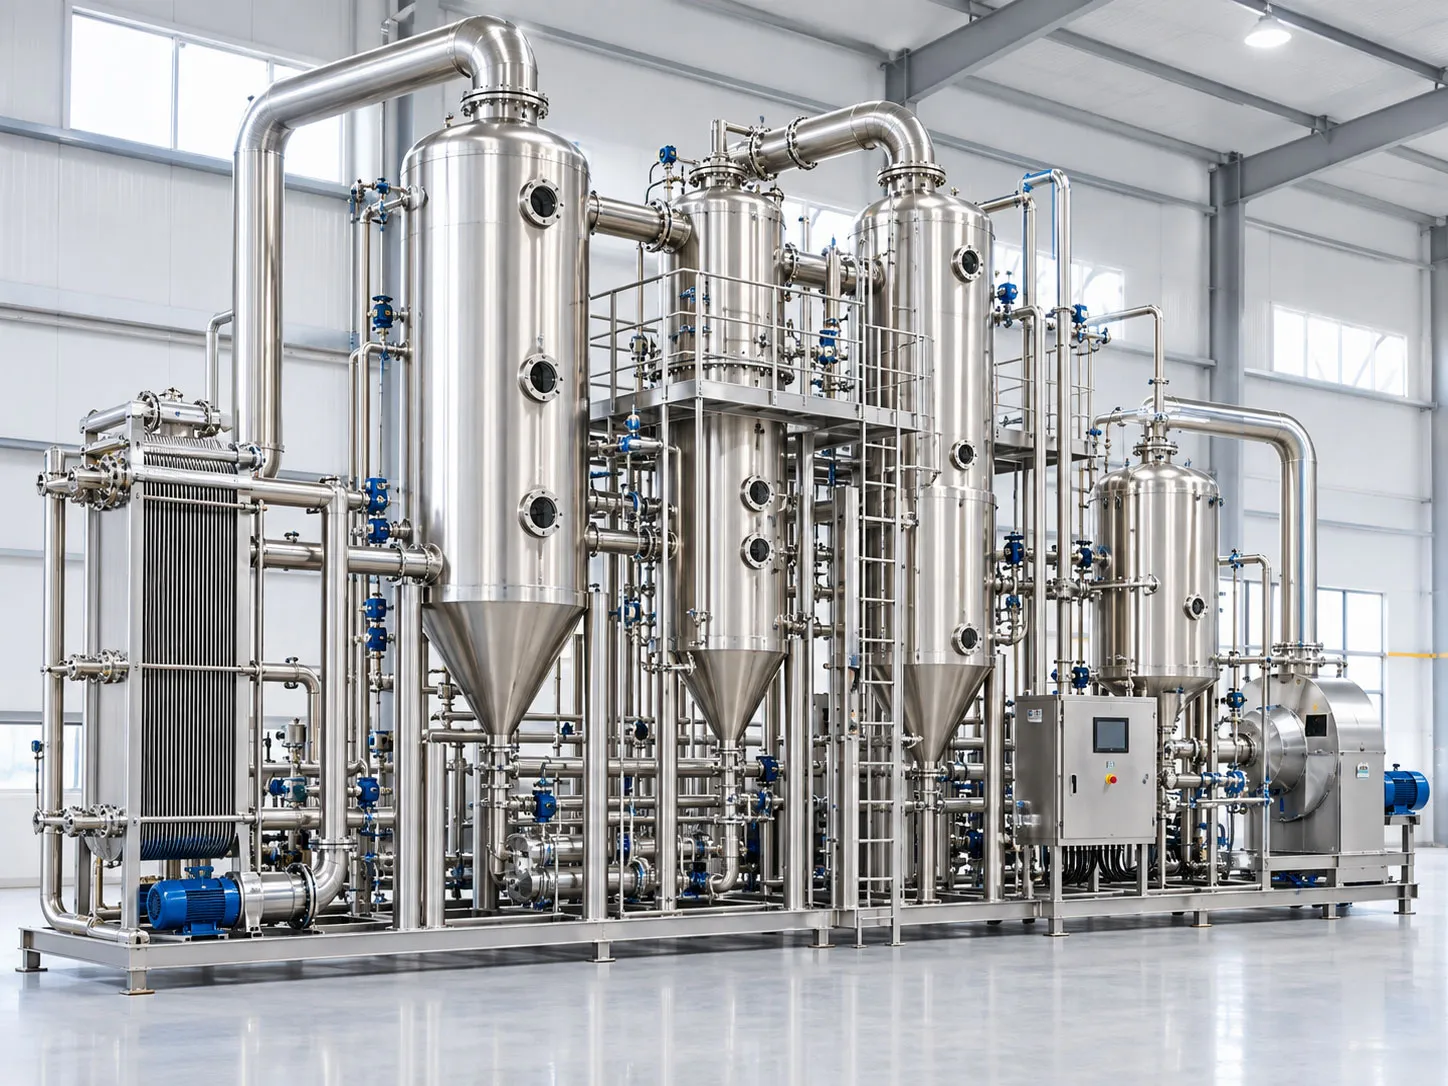
Our Multiple Effect Evaporator (MEE) systems optimize steam efficiency by using the vapor generated from one effect as the heating medium for the subsequent effect. Available in double, triple, and multi-effect configurations, these systems significantly lower operational steam costs in bulk volume concentration.
-
Best For: Large-scale volume reduction, chemical wastewater treatment, and ZLD systems.
-
Key Features: Steam energy recycling, low thermal degradation, and flexible multi-stage configurations.
2. MVR Evaporators (Mechanical Vapor Recompression)
Mechanical Vapor Recompression (MVR) evaporators recompress the evaporated vapor using a mechanical compressor, raising its pressure and temperature to reuse it as the heating steam. MVR systems drastically reduce boiler steam requirements, making them the most energy-efficient solution available.
-
Best For: Continuous operation plants looking to lower steam utility expenses by up to 80–90%.
-
Key Features: Minimal live steam usage, lower carbon footprint, and automated PLC/SCADA controls.
3. Falling Film Evaporators
Engineered for heat-sensitive liquids and low-viscosity solutions, our Falling Film Evaporators pass liquid downwards along inner tube walls to create a thin, rapid-evaporating film.
-
Best For: Food processing, dairy, pharmaceuticals, and heat-sensitive chemical solutions.
-
Key Features: Short residence time, high heat-transfer coefficients, and low temperature differentials.
4. Forced Circulation Evaporators
Designed specifically for high-viscosity, scaling, or crystallizing liquids, Forced Circulation Evaporators rely on high-capacity axial flow pumps to circulate liquid through the heat exchanger tubes at high velocity.
-
Best For: Effluent concentration with high dissolved solids, crystallizers, and heavy chemical slurry.
-
Key Features: Highly resistant to tube fouling, handles high viscosity, and easy maintenance.
Technical Specifications & Capabilities
| Parameter | Specification / Range |
| Capacity Range | 500 LPH to 100,000+ LPH (Custom Sized) |
| Material of Construction (MOC) | SS304, SS316, SS316L, Duplex Steel, Titanium, Hastelloy |
| Operating Pressure | Atmospheric or High Vacuum |
| Automation | Semi-Automatic / Fully Automatic (PLC + SCADA Interfaced) |
| Heating Medium | Steam, Thermal Oil, Hot Water, or MVR Recompression |
Key Advantages of AKSH Industrial Evaporators
-
Optimal Energy Efficiency: Thermal architecture engineered to lower specific steam consumption per kg of water evaporated.
-
Fouling & Scaling Resistance: Custom flow velocity and heat surface designs prevent tube choking during continuous runs.
-
Turnkey Engineering: Full-spectrum support—from process calculation and thermal design to fabrication, installation, and commissioning.
-
ZLD Ready: Seamlessly integrates with crystallizers, spray dryers, and RO plants to meet strict environmental standards.
Industries We Serve
Our industrial evaporation plants are deployed across diverse process sectors:
-
Pharmaceuticals & Biotechnology: Concentrating bulk drug extracts and active ingredients.
-
Chemical & Agrochemical: Solvent recovery and high-TDS wastewater handling.
-
Textiles & Dyeing: Wastewater volume reduction and salt recovery.
-
Food & Dairy: Milk, juice, and syrup concentration.
-
Zero Liquid Discharge (ZLD) Plants: Concentrating industrial brine prior to final crystallization.
Frequently Asked Questions
Related Products
Have a project in mind?
Talk to our engineers about your drying, evaporation or turnkey process requirement.