
For many chemical manufacturers, environmental compliance used to mean running an effluent treatment plant well enough to meet discharge limits. That model is under growing pressure. Dye intermediates, agrochemicals, pharmaceuticals, specialty chemicals and pigments all produce wastewater rich in dissolved salts and stubborn organics, and conventional biological treatment struggles to remove either. As regulators, customers and communities focus more on what actually leaves a factory, the last few percent of the treatment chain has become the hardest and most important part to get right.
That last stretch is where evaporation and spray drying come in. They are the thermal technologies that can take a concentrated, difficult liquid and turn it into recovered water and a dry, manageable solid. This article explains why these two processes have become the final frontier of chemical plant compliance, how they fit into a modern effluent scheme and what plant teams should consider when designing them.
Why Traditional Treatment Is No Longer Enough
Conventional effluent treatment was designed mainly to reduce suspended solids, oil and biodegradable organic load. It does that well. What it does not do is remove dissolved salts, and it often struggles with refractory organic compounds that resist biological breakdown. In many chemical processes, those are exactly the components that dominate the effluent.
Three trends make this gap harder to ignore:
- Attention to total pollution load: Diluting a strong stream with cleaner water may bring concentrations within limits, but it does not reduce the total quantity of salts and organics released. Regulators increasingly look at load, not just concentration.
- Stricter consent conditions: In India, the Central Pollution Control Board and State Pollution Control Boards set the effluent framework, and for certain sectors and locations consent conditions may call for zero liquid discharge or very tight limits. Requirements vary, so each unit must confirm what applies to it.
- Water scarcity: Industrial clusters in water-stressed regions face pressure to reuse water rather than discharge it.
The result is that many chemical plants now need a way to deal with high-salinity, high-COD streams at their source rather than diluting and discharging them.
The Limits of Membranes
Reverse osmosis is the most energy-efficient way to recover large volumes of water from moderately salty effluent, and it plays a central role in most zero liquid discharge schemes. But membranes have a ceiling. As salt concentration rises, osmotic pressure climbs until it exceeds what the membrane system can practically overcome. Scaling salts, silica and organics also foul membranes as concentration increases.
Beyond that point, the remaining brine still contains a significant volume of water and all the dissolved solids. Something has to take it the rest of the way. Membranes cannot; thermal processes can.
Evaporation: Recovering Water from the Hardest Streams
Evaporation removes water by boiling it off, which means it is not limited by osmotic pressure. It can concentrate brine all the way to saturation and beyond, recovering the vapor as clean condensate for reuse. AKSH's industrial evaporators are built for exactly this kind of duty, in several configurations suited to different liquids.
Multiple Effect Evaporators
Multiple effect evaporators reuse the vapor from one stage to heat the next, so each kilogram of live steam evaporates several kilograms of water. They are robust, handle a wide range of liquids and are well suited to sites with available steam.
Mechanical Vapor Recompression
MVR evaporators compress their own vapor with an electric compressor and reuse it as the heating medium, dramatically reducing live steam demand. For large, continuous effluent duties, this can significantly lower the energy cost of compliance. We explain the principle in our article on how MVR evaporators cut steam costs.
Forced Circulation Evaporators and Crystallizers
Chemical effluents often contain salts that scale or crystallize as they concentrate. Forced circulation designs pump liquid through the heat exchanger at high velocity and suppress boiling in the tubes, keeping crystals off the heat transfer surface. They are the usual choice for the final, most concentrated stage of evaporation.
Why Evaporation Is a Compliance Tool
- It recovers water that can be reused in process, cooling towers or utilities.
- It concentrates salts and organics into a much smaller volume for final treatment.
- It works on streams that biological treatment and membranes cannot handle completely.
- It provides a measurable, controllable step whose performance can be recorded.
Spray Drying: Closing the Loop
Evaporation reduces volume, but a concentrated liquid is still a liquid. To achieve zero liquid discharge, the concentrate must be turned into a solid. Crystallizers and agitated thin film dryers are common choices. For many chemical effluents, spray drying offers distinct advantages.
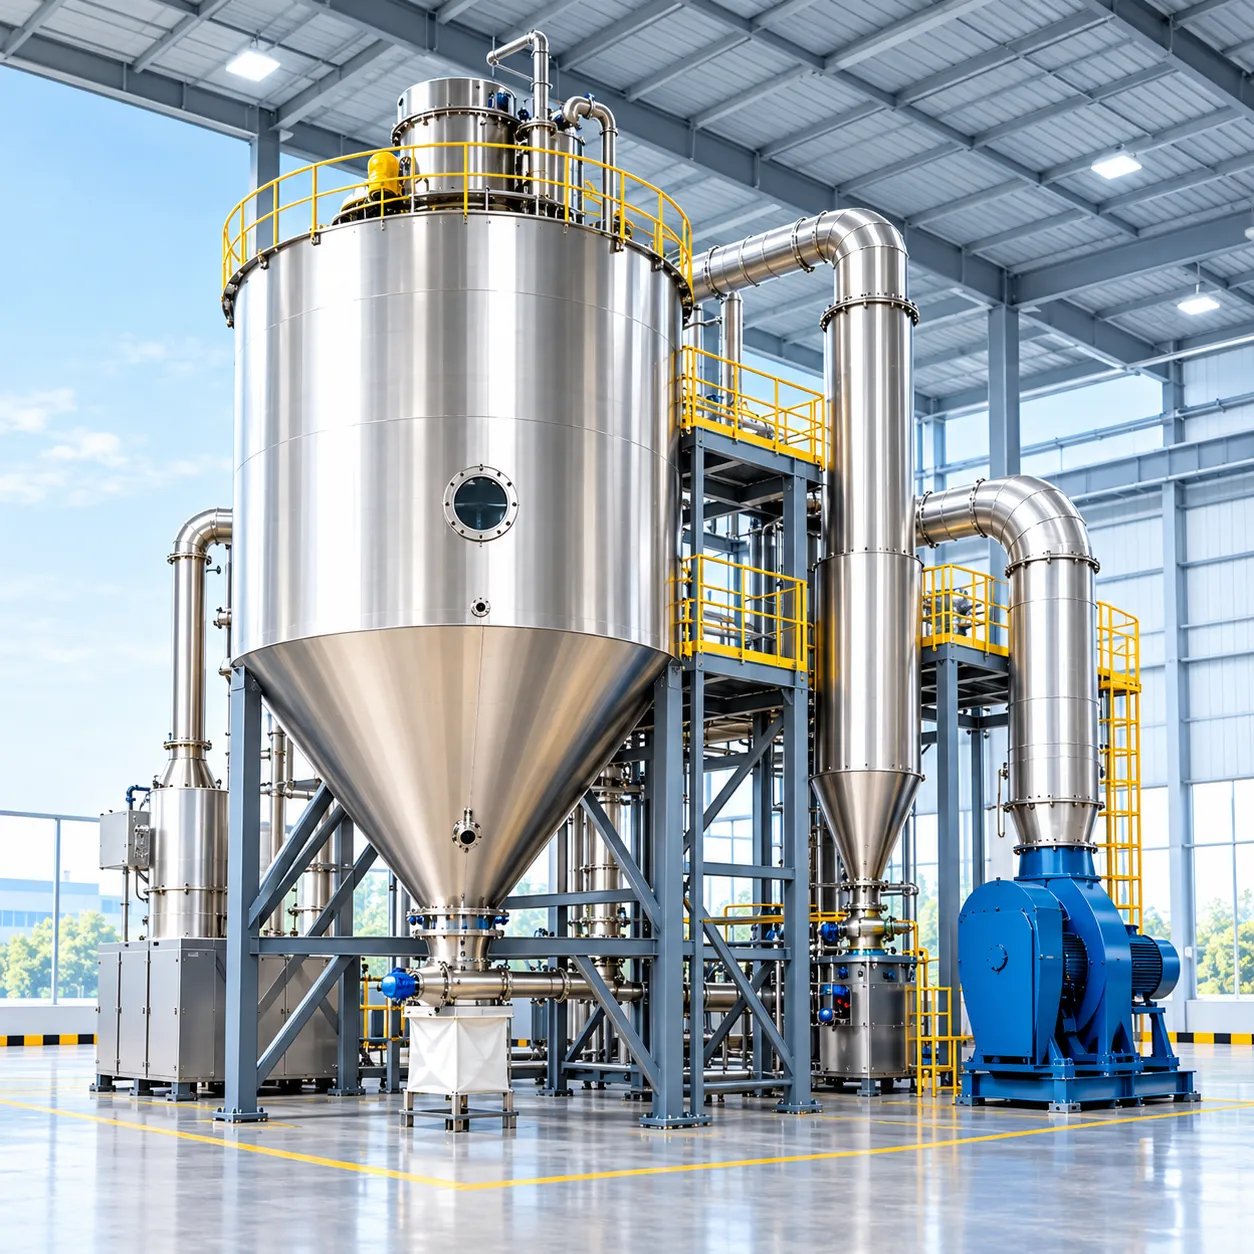
A spray dryer atomizes the concentrate into fine droplets inside a chamber of hot air. The water evaporates within seconds, leaving a dry powder that is collected by cyclones, bag filters or scrubbers. AKSH's industrial spray dryers include heavy-duty effluent and ZLD configurations designed for high-TDS industrial wastewater, dyes and chemical effluent streams.
Where Spray Drying Excels
- Mixed salts and organics: Effluents containing several salts plus organic matter often do not form clean crystals. Spray drying converts the whole concentrate to powder without needing crystallization.
- Sticky or viscous concentrates: Where a crystallizer would struggle, a well-designed spray dryer can often handle the material.
- Continuous operation: Spray dryers run steadily with consistent output, which simplifies downstream handling.
- Compact solid output: A dry powder is easier to pack, store and dispose of than wet sludge or salt cake.
Selecting the right atomizer, chamber size and temperatures for a chemical feed is a specialized task. Our guide on choosing the right spray dryer for chemical slurries covers the main considerations.
How the Pieces Fit Together
A typical compliance-focused scheme for a chemical plant follows a logical sequence. The exact design always depends on the effluent:
| Stage | Typical Technology | Compliance Role |
|---|---|---|
| Segregation and equalization | Separate collection of high- and low-strength streams, holding tanks | Keeps difficult streams concentrated and manageable |
| Pretreatment | Neutralization, filtration, oil removal, softening, organic reduction | Protects membranes and evaporators from fouling |
| Membrane concentration | Reverse osmosis | Recovers water at low energy where salinity allows |
| Thermal evaporation | MEE, MVR, forced circulation | Concentrates brine beyond membrane limits and recovers condensate |
| Solids recovery | Spray dryer, crystallizer, ATFD | Converts concentrate into dry solid, eliminating liquid discharge |
| Air emission control | Cyclones, bag filters, wet scrubbers | Ensures the drying stage does not create an air emission problem |
AKSH's ZLD plants integrate pretreatment, high-recovery RO, MEE or MVR evaporation and final solids recovery into one engineered system. To understand how such schemes compare economically with conventional treatment, read our cost-benefit comparison of ZLD and conventional effluent treatment.
Do Not Trade a Water Problem for an Air Problem
Thermal treatment moves pollutants from one place to another. A spray dryer that is not properly fitted with emission controls can release fine particles to the atmosphere, and vapors from evaporators may carry volatile compounds. A truly compliant design treats air, water and solid waste together.
AKSH's pollution control systems include pulse-jet bag filters, cyclones and wet scrubbers designed to integrate with spray dryers and other thermal equipment, capturing fine powder and scrubbing acidic or soluble gases. The right combination depends on the particle size, temperature, moisture and chemistry of the exhaust. Our article on cyclone separators vs bag filters vs scrubbers explains how to choose.
Design Considerations for Compliance-Grade Thermal Systems
Know the Effluent in Detail
Chemical effluents vary widely between products and even between batches. A detailed analysis of TDS, COD, specific salts, silica, volatile organics, pH and variability is the foundation of any reliable design. Laboratory evaporation and drying trials reduce risk for unfamiliar streams.
Choose Materials for the Concentrated Liquid
As effluent concentrates, chlorides and acids become far more aggressive. Evaporators, separators and dryers may need SS316L, duplex steel, titanium or nickel alloys. Material choice should be based on the final concentrated stream, not the dilute feed.
Manage Fouling and Scaling
Scaling salts and organic residues can rapidly foul heat transfer surfaces. Appropriate evaporator types, cleaning provisions and pretreatment are essential to maintain availability, because a ZLD plant with no discharge route must keep pace with production.
Plan for Volatile Components
Solvents and volatile organics can carry over into condensate, affecting its reuse quality. Stripping, condensate polishing or segregated handling may be necessary. Where a concentrate contains flammable solvents, the drying stage itself must be designed for safety, often using an inert gas such as nitrogen in a closed circuit with solvent recovery, so that compliance does not come at the expense of process safety.
Control and Record Everything
Compliance depends not only on performance but on proof of performance. Automated control with data logging records flows, temperatures, recoveries and alarms, providing the documentation inspectors and auditors expect.
Consider Energy From the Start
Thermal treatment is energy-intensive. Maximizing economical RO recovery, segregating dilute streams, choosing MVR where it makes sense and recovering heat from condensate all reduce the running cost of compliance. The cost drivers are explained in our article on what affects ZLD plant cost in India.
Where These Technologies Are Making the Difference
The combination of evaporation and spray drying is relevant across many chemical sub-sectors, each with its own challenges:
- Dyes and dye intermediates: Mother liquors and wash waters carry high salt loads and intense color that biological treatment cannot fully remove.
- Agrochemicals: Process effluents often contain refractory organics and mixed salts that resist conventional treatment.
- Bulk drugs and pharmaceutical intermediates: High-COD, high-salinity streams from synthesis steps, sometimes with solvent traces.
- Pigments and inorganic chemicals: Salt-rich filtrates and wash liquors from precipitation and washing operations.
- Specialty and performance chemicals: Smaller but complex streams that change with each product campaign.
A Practical Roadmap for Plant Teams
Moving from conventional treatment to a thermal compliance scheme is a project in its own right. A structured approach reduces risk:
- Map every stream: Identify sources, volumes and composition of all effluent streams, not just the combined outlet.
- Segregate where possible: Keep high-strength streams apart from dilute ones so each can be treated economically.
- Reduce at source: Review process steps, washing practices and recycling options before sizing treatment equipment.
- Run treatability trials: Test evaporation and drying behavior on real samples to confirm scaling, foaming and powder characteristics.
- Select and size the scheme: Choose membrane, evaporation, drying and emission control stages based on trial data and utility availability.
- Plan solid residue handling: Arrange storage, packing and authorized disposal or recovery routes before commissioning.
- Train and monitor: Prepare operators, set performance indicators and review data regularly with the equipment supplier.
Beyond Compliance: Recovering Value
Evaporation and spray drying are not only end-of-pipe tools. In many chemical plants, the same technologies can recover product from mother liquors, reclaim salts with resale value or return solvents to the process. When a stream that was once a liability becomes a source of recovered water, product or energy savings, compliance spending begins to pay something back. The broader shift toward resource recovery is part of our wider work in sustainability solutions.
Why Choose AKSH Engineering
AKSH Engineering Systems Pvt. Ltd., based in Ahmedabad, Gujarat, has been designing and manufacturing evaporation, spray drying and turnkey process plants since 2013, with more than 100 installations. Our team of technocrats brings over 100 years of combined experience. Because we design and fabricate evaporators, spray dryers and pollution control equipment in-house, we can engineer the thermal end of your effluent scheme as one integrated system rather than a set of separate packages.
Conclusion
Chemical plants can no longer rely on dilution or on treatment that leaves dissolved salts and refractory organics untouched. Membranes recover much of the water, but they reach a hard limit. Evaporation takes the brine beyond that limit and recovers clean condensate, and spray drying or crystallization turns the final concentrate into a dry, manageable solid. Together, with proper air emission control and automation, they close the loop that compliance increasingly demands.
If your plant is facing stricter effluent conditions or planning a zero liquid discharge project, talk to the AKSH Engineering team. We will study your effluent and recommend an evaporation and drying scheme that meets your compliance goals efficiently.