
Every food factory produces a second product line that rarely appears in its sales reports: peels, pulp, pomace, husks, spent grains, trimmings and off-specification batches. Much of this material is more than half water. It is heavy to transport, starts to ferment within hours, attracts flies and odor complaints, and costs money to dispose of. For many processors, it is simply a cost center that grows with production.
Drying changes the equation. Once moisture is removed, the same material becomes light, stable and storable, and it can be sold as animal feed, used as a fuel, blended into fertilizers or refined into ingredients. Rotary dryers are among the most practical machines for this transformation, because they handle bulky, wet and variable residues at the scale food plants generate them. This article looks at food waste drying from a business and engineering perspective: which streams are worth drying, what products they can become, how a rotary drying line is put together and what to watch out for.
Why Food Waste Is a Drying Problem
Food processing residues share a few characteristics that make them hard to manage in their wet state:
- High moisture: Many fruit and vegetable residues contain 70 to 90% water, and pressed spent grains often hold 60% or more.
- Rapid biological activity: Sugars and proteins support microbial growth, so wet residues spoil, ferment and smell quickly, especially in warm climates.
- Low bulk value when wet: Transporting a truckload that is mostly water rarely makes economic sense, so wet residues are often given away or landfilled.
- Seasonality: Fruit, vegetable and sugar processing peaks during harvest, creating short periods of very high waste volume.
Reducing moisture to roughly 10 to 12%, a common target for storage stability, arrests microbial activity, cuts weight by a large factor and turns a perishable liability into a commodity that can be stored, shipped and sold.
Food Waste Streams and What They Can Become
Not every residue has the same value. The table below summarizes common streams, typical moisture levels and the products they can be converted into. Moisture figures vary widely with process and season and are indicative only.
| Waste stream | Typical moisture as generated | Possible dried products |
|---|---|---|
| Citrus peel and pulp | Often 75 to 85% | Cattle feed pellets, feedstock for pectin and fiber extraction |
| Brewers and distillers spent grains | Often 60 to 80% | High-protein feed ingredient, food-grade fiber and protein flour |
| Fruit pomace (apple, grape, tomato) | Often 65 to 80% | Feed, dietary fiber, seed recovery, natural pigment feedstock |
| Vegetable trimmings and peels | Often 80 to 90% | Feed supplement, compost and organic fertilizer base |
| Cassava and starch processing residue | Often 60 to 80% | Feed ingredient, fermentation substrate |
| Bakery and snack rejects | Often 10 to 40% | Energy-rich feed ingredient |
| Fish and poultry processing byproducts | Often 60 to 75% | Protein meals for feed (after cooking and pressing) |
The Main Value Pathways
Animal feed
The largest and most established outlet. Dried citrus pulp, distillers grains, bakery meal and fruit pomaces are traded as feed ingredients in many countries. They supply energy, fiber and in some cases protein. Feed buyers expect consistent moisture, freedom from mold and contamination, and predictable nutrient composition, which is why controlled drying matters more than simple dehydration.
Food ingredients and extraction feedstock
Some residues contain valuable components: pectin in citrus peel, dietary fiber in fruit pomace and spent grain, polyphenols in grape pomace, and protein in brewers grain. Drying stabilizes the material so it can be stored and transported to an extraction plant, or milled into fiber and flour products. These outlets usually command higher prices than feed but demand stricter hygiene and gentler temperatures.
Fuel
Dried husks, shells, pomace and some fibrous residues can be burned in biomass boilers or pelletized as fuel. A plant may even use part of its dried waste to fire the dryer itself, closing the energy loop.
Fertilizer and soil amendment
Residues with lower feed value can be dried and granulated into organic fertilizers or blended with mineral nutrients. Drying reduces volume and odor and makes the material easier to spread or bag.
Why Rotary Dryers Suit Food Waste
Several dryer types can process food residues, but rotary dryers have particular advantages for this duty:
- Tolerance of irregular, fibrous and lumpy material: Peels, husks and pulp do not need to be finely ground before entering the drum.
- Capacity for seasonal peaks: A single drum can handle large tonnages continuously, matching the volumes generated during harvest campaigns.
- Handling of sticky phases: By mixing a portion of dried product back into the wet feed, the drum can carry sugary or pulpy residues through their sticky phase without heavy buildup.
- Flexible heating: Direct firing, clean hot air from a steam or thermic fluid air heater, or indirect heating can be chosen to suit the product's end use and contamination limits. Our guide to direct vs indirect heating in rotary dryers explains how to choose.
- Robustness: Food waste is variable and may contain stones or tramp metal. A heavy-duty drum is far more forgiving than a delicate dryer.
Rotary dryers are used for many other bulk materials too, as described in our overview of the top applications of rotary dryers across industries. Food waste valorization is one of the faster-growing areas.
Building a Food Waste Drying Line: Step by Step
A successful plant is more than a dryer. A typical line follows this sequence:
- Collection and reception: Residues are collected promptly to limit spoilage, inspected and fed into a covered receiving hopper. Foreign material such as plastics and metal is removed.
- Size reduction: Large pieces such as whole fruit or cabbage leaves are shredded to a consistent size so they dry evenly.
- Mechanical dewatering: Screw presses, belt presses or decanters remove as much free water as practical. This is the most important energy-saving step, because mechanical water removal costs far less than thermal evaporation.
- Handling the press liquor: The liquid pressed out often contains dissolved sugars and solids. Rather than discharging it, many plants concentrate it in industrial evaporators and blend the concentrate back with the solids, raising yield and reducing effluent.
- Back-mixing: For sticky residues, part of the dried product is recycled and mixed with the wet feed to create a crumbly, granular mixture.
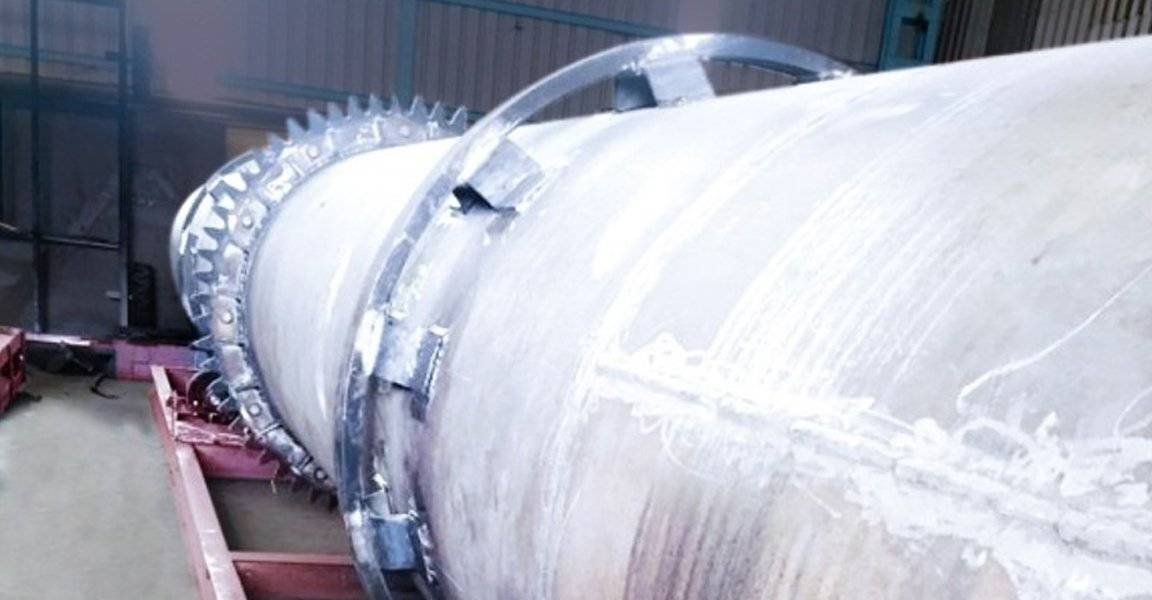
- Rotary drying: The prepared feed is dried in a co-current drum where the hottest gas meets the wettest material, keeping product temperatures moderate.
- Cooling and conditioning: Dried material is cooled to prevent condensation and caking in storage.
- Milling, pelleting or bagging: The product is finished into the form the market wants: meal, pellets, fiber powder or bulk.
- Exhaust treatment: Dust and odor are captured before discharge.
A Worked Example: Why Dewatering Comes First
Consider a juice plant producing 20 tons per day of citrus peel and pulp at around 82% moisture. The dry solids amount to about 3.6 tons. If that material went straight into a dryer and left at 10% moisture, the product would weigh roughly 4 tons, so the dryer would have to evaporate about 16 tons of water every day.
Now suppose the peel is first treated and pressed down to around 65% moisture, a step commonly used in citrus pulp plants. For simplicity, ignore the small share of solids that leaves with the press liquor; in practice some dissolved sugars do escape this way, which is exactly why plants try to recover them, as described below. On that simplified basis, the same 3.6 tons of solids now arrive in about 10.3 tons of pressed cake, and the dryer needs to evaporate only about 6.3 tons of water to reach the same product. That is a reduction of more than half in evaporation load, which translates directly into a smaller drum, smaller fans and much lower fuel use. The press liquor, rich in dissolved sugars, can then be concentrated and blended back to recover solids that would otherwise be lost.
The numbers are illustrative, but the principle holds for almost every wet food residue: invest in removing water mechanically before paying to remove it thermally.
Quality, Safety and Regulatory Points
When dried residues go into feed or food chains, the product must be safe and traceable. Processors should keep each residue stream segregated, avoid mixing in packaging or non-food material, and document drying temperatures and moisture results for each lot. Clean, single-source processing residues are generally far easier to market than mixed post-consumer food waste, which is subject to stricter rules in many jurisdictions. Local feed, fertilizer and pollution control regulations should be checked early, because they shape both the equipment specification and the market for the dried product.
Engineering Challenges and How to Address Them
Stickiness and buildup
Sugary residues such as citrus and fruit pomace become tacky as they dry. Back-mixing, co-current flow, special flights near the feed end and knockers on the shell all help. Getting the recycle ratio right is often a matter of trials.
Odor and emissions
Drying food residues releases odorous volatiles along with dust. Exhaust is typically cleaned with cyclones and then a wet scrubber or bag filter, and odor control may need additional treatment. AKSH supplies integrated pollution control systems, and our comparison of cyclone separators, bag filters and scrubbers helps match equipment to exhaust conditions.
Fire risk
Dry organic dust and fines are combustible. Temperature control, spark detection, explosion venting where appropriate and reduced oxygen through exhaust recirculation lower the risk.
Product quality for feed and food
Overheating can reduce protein digestibility, darken color and destroy valuable compounds. Moderate outlet temperatures, short exposure of dry material to hot gas and good moisture control protect value.
Energy cost
Because food residues are so wet, energy is the largest operating cost. Mechanical dewatering, waste heat use, insulation and exhaust recirculation all matter, and several of the newer techniques are covered in our piece on innovations boosting energy efficiency in rotary drying systems. Our article on zero-waste drying and reducing energy costs discusses whole-plant energy strategies.
When a Different Dryer Makes Sense
Rotary drums are not the only option. Fine, pasty residues such as protein-rich filter cakes or pectin-bearing precipitates may be better dried in a swirl agitated spin flash dryer, which breaks up cohesive cakes and dries them in seconds. Liquid side streams, such as whey or fruit juices, are spray dried. Choosing the right combination often produces higher-value products than forcing everything through one machine.
Building the Business Case
Before investing, processors should answer a few questions honestly:
- How many tons of each residue are generated per day and per season, and at what moisture?
- What does disposal cost today, including transport, landfill or third-party fees?
- Is there a reliable buyer for the dried product, and at what specification and price?
- What heat sources are available on site, such as surplus steam, boiler flue gas or biomass?
- What are the local emission and odor requirements?
The strongest projects usually combine avoided disposal cost, product revenue and reduced environmental risk. Drying also supports broader sustainability goals, which our sustainability solutions range addresses across water and waste.
Why AKSH Engineering
AKSH Engineering Systems Pvt. Ltd. has designed and manufactured drying and evaporation systems in Ahmedabad, Gujarat, since 2013, with more than 100 installations. Our rotary dryers are built in-house in direct-fired and indirect-fired versions, with custom flight designs for sticky and fibrous feeds, insulated shells, sealed ends and variable speed drives. Because we also manufacture evaporators, spin flash dryers, spray dryers and dust collection equipment, our team of technocrats, with over 100 years of combined experience, can design the complete chain from wet residue to finished product.
Conclusion
Food processing residues do not have to be a disposal headache. With good mechanical dewatering, a well-designed rotary dryer and proper exhaust treatment, peels, pulp, pomace and spent grains can become feed ingredients, fiber, fuel or fertilizer, often turning a cost center into a modest revenue stream while reducing environmental impact.
If your plant generates wet food residues and you want to explore whether drying makes sense, contact the AKSH Engineering team. Share your waste volumes and characteristics, and our engineers will help you evaluate the options and design a practical valorization line.