
Rotary dryers are among the most robust machines in process industry, but they are also among the hungriest for energy. A large drum drying sand, fertilizer or biomass can burn through fuel worth many times its own purchase price over its working life. With fuel prices volatile, emission rules tightening and customers asking about carbon footprints, the energy performance of a rotary drying system has moved from an operating detail to a boardroom topic.
The good news is that rotary drying technology has not stood still. Improvements in heat recovery, combustion, mechanical design, sensing and automation now allow new installations to use noticeably less energy than older designs, and many of the same ideas can be retrofitted to existing drums. This article explains where energy is lost in a rotary dryer and walks through the innovations that are delivering real savings today.
Where the Energy Goes in a Rotary Dryer
Before discussing solutions, it helps to know where the heat ends up. In a typical direct-fired rotary dryer, the heat input is split between several destinations:
- Evaporating water: The useful work. Each kilogram of water needs its latent heat, typically around 2,300 to 2,500 kJ depending on conditions, plus the heat to bring it to evaporation temperature.
- Exhaust gas losses: Warm, humid gas leaving the stack carries away sensible heat. This is usually the largest single loss.
- Heating the product: The dried solids leave warmer than they entered, and that heat is often lost in storage or cooling.
- Shell and surface losses: Radiation and convection from the drum shell, ducts and burner housing.
- Air leakage: Cold ambient air drawn in at poor seals dilutes the hot gas, cools it, and must then be heated and moved by the fan.
- Electrical energy: Drum drive, fans, conveyors and dust collectors.
Every innovation discussed below targets one or more of these losses. For a step back to the fundamentals of how the drum moves and dries material, see our article on how rotary dryers improve efficiency in agriculture and food processing, which also includes a simple evaporation-load calculation.
1. Exhaust Gas Recirculation
Instead of sending all exhaust gas to the stack, a portion is returned to the burner chamber and mixed with fresh combustion gas. Because the recycled gas is already warm, less fuel is needed to reach the target inlet temperature. Recirculation also lowers the oxygen content inside the drum, which reduces fire risk with combustible dusts, and it can help some products dry more gently at higher humidity.
The limit is moisture: if too much humid gas is recycled, the drying driving force falls and the drum loses capacity. Modern systems use humidity or dew point measurement to set the recirculation ratio, rather than a fixed damper position.
2. Heat Recovery from Exhaust
Where recirculation is unsuitable, heat exchangers can recover energy from the exhaust after dust collection. Air-to-air exchangers preheat combustion air or drying air, while air-to-liquid exchangers heat water or thermic fluid for use elsewhere in the plant, such as feed preheating or space heating.
The practical challenges are dust and condensation. Exhaust from dryers often carries fines and moisture that can foul heat exchanger surfaces, so recovery equipment is placed downstream of efficient cyclones and bag filters, and designed with cleaning access. Pairing the dryer with well-designed pollution control systems is therefore not only an emission requirement but also a precondition for effective heat recovery.
3. Using Waste Heat from Other Processes
Many plants already produce hot gas they do not use: flue gas from boilers, kilns, furnaces, engines or thermal oxidizers. A rotary dryer can be designed to accept this gas directly or through a heat exchanger, sometimes with a small supplementary burner for control. In biomass and cement-adjacent industries, drying fuel or raw material with waste kiln or boiler gas is one of the most cost-effective energy measures available. Integrating heat across the whole site in this way is a core idea in our article on zero-waste drying and reducing energy costs in industrial processing.
4. Better Burners and Combustion Control
Combustion technology has advanced considerably. Modern burners offer wide turndown, so they can operate efficiently at low loads rather than cycling on and off. Oxygen trim control measures residual oxygen in the flue gas and adjusts the air-to-fuel ratio continuously, avoiding the excess air that wastes heat. Multi-fuel burners allow switching between gas, oil and biomass-derived fuels according to cost and availability. Each of these reduces fuel per ton of water evaporated without changing the drum itself.
5. Smarter Flight Design
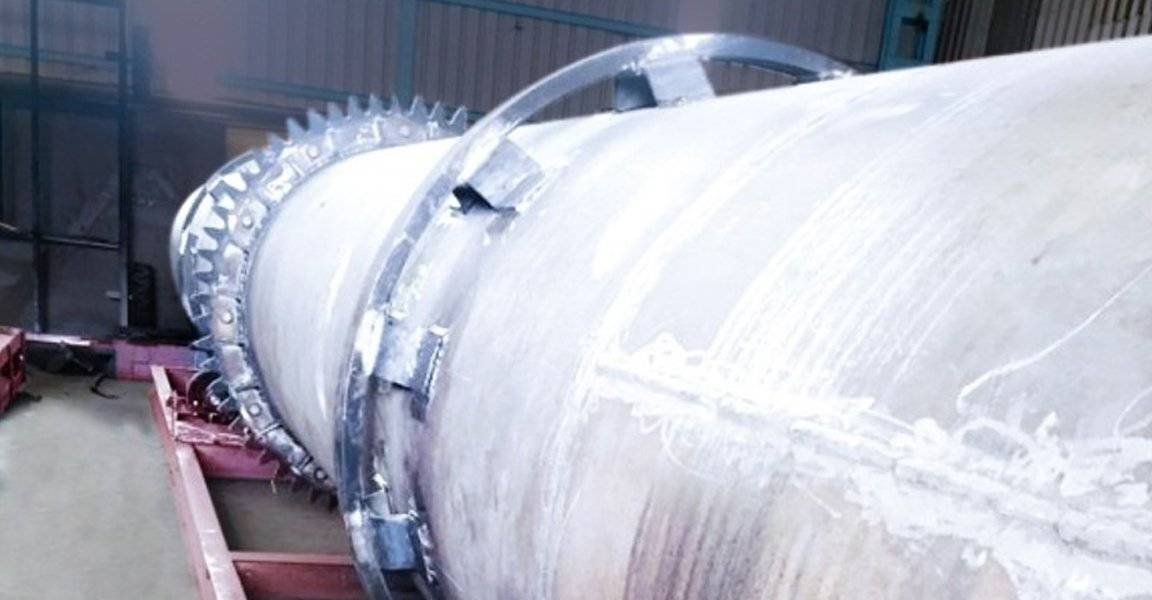
The flights inside the drum decide how well the material curtain fills the gas stream. Too sparse a curtain lets hot gas bypass the product; too dense a curtain creates dust and pressure drop. Engineers now use particle modeling and practical experience to design flight profiles that change along the drum length: special flights near the feed end for sticky wet material, lifting flights in the main drying zone, and gentle flights near discharge to limit attrition. A well-filled curtain extracts more heat from the gas before it leaves, which directly lowers exhaust temperature and fuel use.
6. Improved Insulation and Sealing
Two of the simplest innovations are also among the most effective. High-performance insulation and cladding on the drum, burner housing and ducts cut surface losses. Modern seal designs at the feed and discharge ends, such as spring-loaded leaf seals, graphite block seals and labyrinth arrangements, dramatically reduce tramp air leakage. Lower leakage means a smaller fan load, more stable temperatures and less fuel. On older drums, seal and insulation upgrades are often the fastest retrofit payback.
7. Variable Speed Drives
Fixed-speed drums and fans cannot respond to changing feed conditions. Variable speed drives (VFDs) on the drum let operators adjust residence time as feed moisture changes. VFDs on induced draft and combustion air fans match airflow to the actual load rather than throttling with dampers, which can cut fan power substantially at part load, since fan power falls steeply as speed is reduced.
8. Inline Moisture Measurement
Many dryers still rely on outlet gas temperature alone, with occasional lab samples. Inline moisture sensors based on near-infrared, microwave or capacitance principles measure product moisture continuously at the dryer discharge or even at the feed. With real-time moisture data, the control system can hold the product just inside specification instead of over-drying as a safety margin. Because over-drying wastes energy on every ton, tighter moisture control is one of the most valuable efficiency tools available.
9. Advanced Automation, Analytics and Digital Twins
PLC and SCADA systems now coordinate burner, fans, drum speed, feed rate and recirculation from a single interface, with recipes for different products and full data logging. Beyond basic loops, model-based control uses a dynamic model of the dryer to anticipate disturbances such as a change in feed moisture, adjusting heat input before product quality drifts. Digital twins extend this to scenario testing and operator training. Our instrumentation, automation and controls packages are built on this approach, and our articles on how PLC and SCADA automation improves dryer consistency and future trends in industrial drying with AI and digital twins explore the direction of travel.
10. Predictive Maintenance
Mechanical condition affects energy. Misaligned trunnions increase drive power, worn seals let in air, and damaged flights reduce heat transfer. Vibration sensors, temperature monitoring of bearings and shell, and periodic thermal imaging allow maintenance teams to spot problems early and schedule repairs before efficiency and reliability fall.
11. Better Mechanical Dewatering Upstream
The cheapest water to remove is the water that never reaches the dryer. Improved screw presses, filter presses, centrifuges and decanters can lower feed moisture significantly at a fraction of the energy cost of thermal evaporation. Even a few points of moisture removed mechanically reduce the evaporation load and allow a smaller dryer or higher throughput.
12. Staged and Hybrid Drying
Instead of asking one drum to take material all the way from very wet to bone dry, some lines split the job. A rotary dryer removes the bulk of the moisture efficiently, and a continuous fluid bed dryer finishes and cools the product with precise moisture control. Each stage operates in its most efficient range, and the overall system can use less energy than a single oversized drum.
13. Cleaner and Renewable Heat Sources
Energy efficiency and energy cost are not the same thing. Some plants are reducing both cost and emissions by changing what supplies the heat. Biomass-fired hot air generators burning husk, bagasse or wood residue are common in agro regions. Solar thermal preheating of drying air is being trialed for low-temperature duties. Where low-pressure steam is surplus on site, a steam air heater can replace part of the fossil fuel input. The best choice depends on fuel availability, emission rules and how stable the heat supply is.
Measuring Success: The KPIs That Matter
Innovations only pay off if their effect is measured. Three indicators give a clear picture of rotary dryer performance:
- Specific heat consumption: Heat input in kJ or kcal per kilogram of water evaporated. This is the core efficiency figure, independent of throughput.
- Specific power consumption: Electrical kWh per ton of product, covering drum drive, fans and auxiliaries.
- Moisture consistency: The spread of final moisture around the target. A narrower spread allows a target closer to the specification limit and less over-drying.
Tracking these figures before and after each change shows which measures deliver real savings and builds the case for the next investment.
Summary Table of Efficiency Innovations
| Innovation | Loss it targets | Retrofit potential |
|---|---|---|
| Exhaust gas recirculation | Exhaust heat loss | Moderate, needs ducting and controls |
| Exhaust heat recovery | Exhaust heat loss | Moderate, depends on dust and space |
| Waste heat integration | Fuel input | High where hot gas is available nearby |
| Modern burners and oxygen trim | Excess air, poor turndown | High |
| Optimized flight design | Gas bypass, high exhaust temperature | High during shutdowns |
| Insulation and seal upgrades | Surface loss, air leakage | Very high, often fastest payback |
| Variable speed drives | Fan and drive power, over-drying | Very high |
| Inline moisture measurement | Over-drying | High |
| Advanced automation and digital twins | Process variability | High, builds on existing PLC |
| Upstream dewatering | Evaporation load | Depends on feed type |
A Practical Roadmap for Your Plant
- Measure first: Record fuel, power, feed rate, feed and product moisture, inlet and outlet temperatures and exhaust oxygen for a representative period.
- Calculate specific energy: Work out heat input per kilogram of water evaporated and compare it with the theoretical minimum.
- Fix the basics: Repair seals and insulation, tune combustion and correct over-drying.
- Add control capability: Install VFDs, inline moisture measurement and better automation.
- Invest in recovery: Evaluate recirculation, heat exchangers and waste heat integration with a clear payback analysis.
- Rethink the process: Consider upstream dewatering, staged drying or a different heating method. Our guide to direct vs indirect heating in rotary dryers may help when the heating method itself is in question.
Why AKSH Engineering
AKSH Engineering Systems Pvt. Ltd., based in Ahmedabad, Gujarat, has designed and built industrial drying and evaporation systems since 2013, with more than 100 installations. Our rotary dryers are manufactured in-house with integrated thermal insulation, sealed feed and discharge housings, custom flight geometry and variable speed drives, and can be heated by direct gas or oil firing, steam air heaters, thermic fluid or hot flue gas. Our team of technocrats, with over 100 years of combined experience, also supplies dust collection and automation, and our wider sustainability solutions help plants reduce resource use across the process.
Conclusion
Rotary drying will always be energy intensive, but it no longer has to be wasteful. Heat recovery, waste heat integration, modern combustion, better flights, tight seals, variable speed drives, inline moisture measurement and intelligent automation each chip away at losses, and together they can transform the economics of a drying line. The most effective programs start with measurement and fix the basics before moving to larger investments.
If you want to cut the energy cost of an existing rotary dryer or specify an efficient new system, contact the AKSH Engineering team. We will review your operating data and recommend the improvements that make the most sense for your material and your plant.