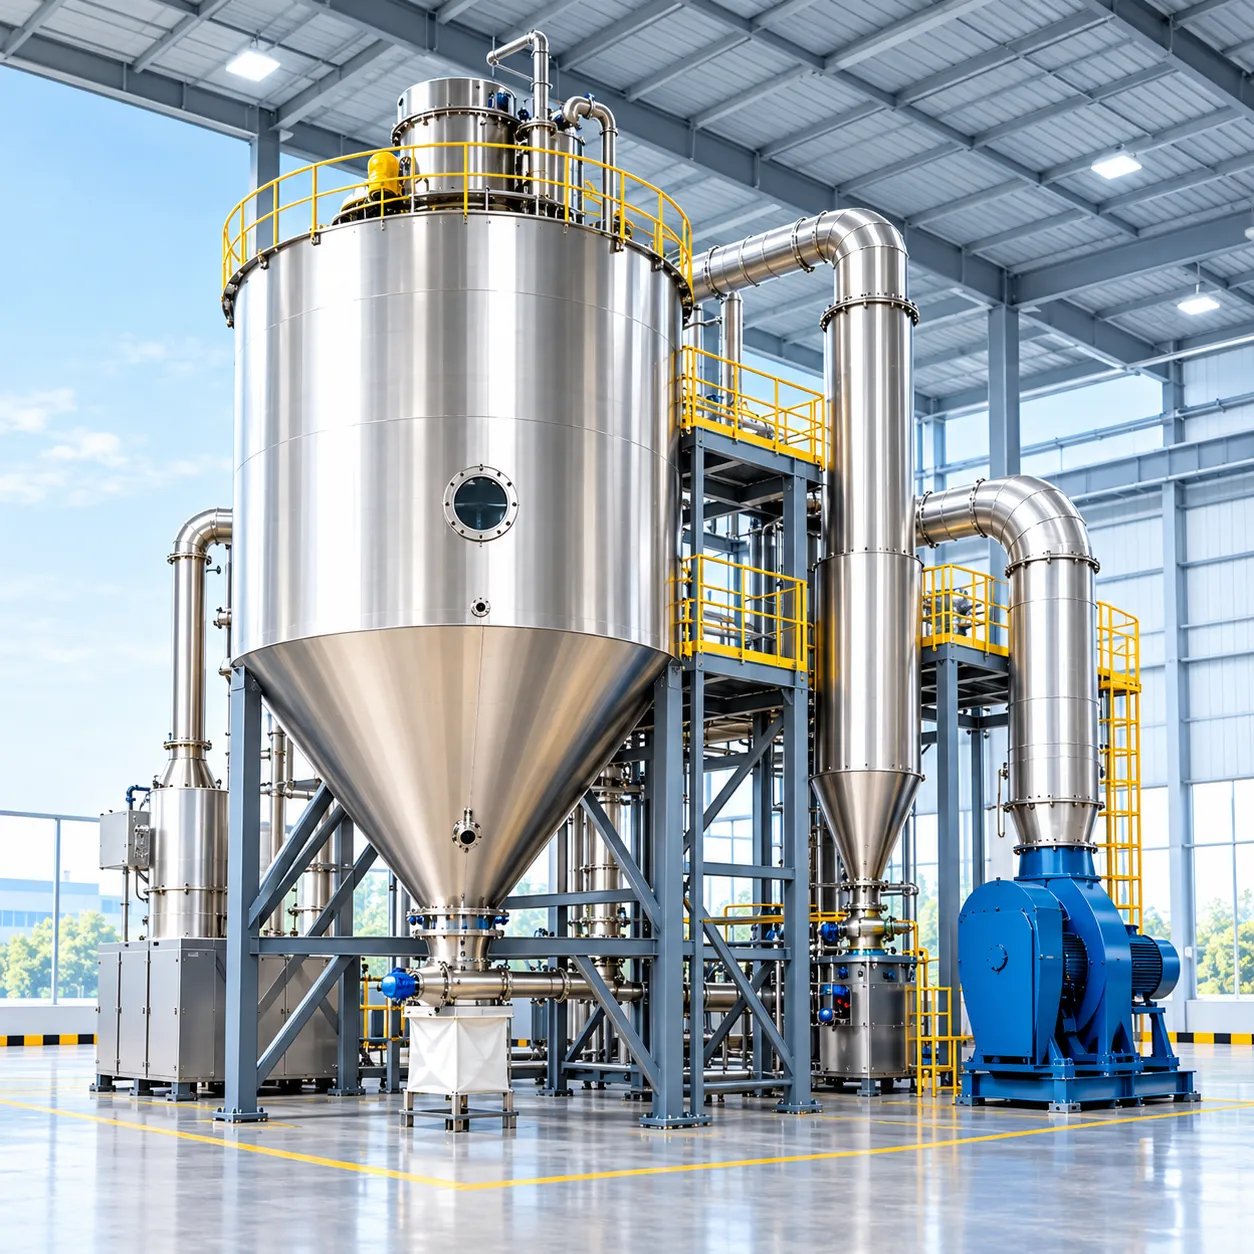

Spray drying is one of the most energy-intensive unit operations in a powder plant. Removing water by evaporation always needs a large amount of heat, and a spray dryer does this with hot air that leaves the plant still carrying much of the energy that went into it. For dairy, food, chemical and pharmaceutical manufacturers, the dryer's fuel or steam bill is often one of the largest operating costs on site, and it rises every time fuel prices do.
The good news is that spray dryer energy use is not fixed. It depends on the feed, the temperatures, the plant configuration, the condition of the equipment and the way it is operated. This guide sets out practical energy-saving tips for industrial spray dryers, from quick operational wins to larger design upgrades, so plant heads and process engineers can prioritize the changes that suit their budget and product.
Understanding Where the Energy Goes
Before improving efficiency, it helps to understand the heat balance. The energy supplied by the air heater is used in several ways:
- Evaporating water: the useful duty. Each kilogram of water needs roughly 2,300 to 2,500 kJ of latent heat, depending on conditions.
- Heating the product and feed: sensible heat to raise solids and remaining moisture to the outlet temperature.
- Exhaust losses: the hot, humid exhaust air leaving the plant, usually the largest single loss.
- Radiation and convection losses: heat escaping through the chamber walls, ducts and cyclones.
- Air leaks: cold air drawn into the system that must be heated or that dilutes the drying air.
A useful rule of thumb for comparing operating conditions is the approximate thermal efficiency of the drying air:
Efficiency ≈ (inlet temperature - outlet temperature) / (inlet temperature - ambient temperature)
For example, a dryer running at 200°C inlet, 90°C outlet and 30°C ambient has an approximate efficiency of 110/170, or about 65%. Raising the inlet to 220°C while holding the same outlet increases this to about 68%. The formula is simplified, but it shows clearly why inlet and outlet temperatures are the two biggest levers. For the underlying science, see our article on the physics of spray drying and heat and mass transfer.
Tip 1: Concentrate the Feed Before It Reaches the Dryer
The single most effective energy-saving step is often to remove more water before spray drying. Evaporators, especially multiple-effect and mechanical vapor recompression designs, remove water at a fraction of the energy cost per kilogram that a spray dryer needs, because they reuse the heat in the vapor.
The effect of higher solids is larger than many people expect. Consider a feed concentrated from 30% to 45% solids:
| Feed Solids | Water per kg of Dry Solids | Change in Water to Evaporate |
|---|---|---|
| 30% | About 2.33 kg | Baseline |
| 40% | About 1.50 kg | About 36% less |
| 45% | About 1.22 kg | About 48% less |
| 50% | 1.00 kg | About 57% less |
The practical limit is viscosity: very concentrated feeds can be difficult to pump and atomize evenly. Feed heating, suitable atomizers and pilot trials help find the highest workable solids content. AKSH designs industrial evaporators for this kind of pre-concentration duty, and our article on how MVR evaporators cut steam costs explains why evaporation is so much more efficient than drying.
Preheat the Feed
Warming the feed with low-grade waste heat, such as hot condensate or process water, reduces the sensible heat that must be supplied in the chamber and often lowers viscosity, which improves atomization. Feed temperature must stay below the point at which the product degrades, thickens or crystallizes.
Tip 2: Run at the Highest Safe Inlet Temperature
A higher inlet temperature means each kilogram of air carries more drying capacity, so less air must be heated and moved for the same evaporation. The upper limit depends on the product's heat sensitivity, its tendency to scorch or discolor, and dust explosion considerations. Because droplets are cooled by evaporation, many products tolerate higher inlet temperatures than their bulk heat sensitivity would suggest, but this should always be confirmed by trials and product testing.
Tip 3: Lower the Outlet Temperature Where Possible
The outlet temperature is closely linked to final powder moisture: a higher outlet gives a drier powder but sends more heat up the stack. Many plants run with a safety margin that is higher than the product actually needs. Reducing the outlet temperature step by step, while monitoring powder moisture and stickiness, can deliver worthwhile savings with no capital cost.
Use Multistage Drying
Multistage drying takes this idea further. The powder leaves the main chamber slightly moist at a lower outlet temperature and finishes drying in a fluid bed, where residence time is longer and the air demand is lower. According to AKSH's product data, multistage spray dryers operating with higher inlet and lower exhaust temperatures can cut specific steam and fuel consumption by up to 15 to 25% compared with single-stage designs, while also producing agglomerated, less dusty powders.
Tip 4: Recover Heat From the Exhaust
Exhaust air typically leaves the plant warm and humid, and recovering part of that heat is one of the larger design-level savings. Common approaches include:
- Air-to-air heat exchangers that transfer heat from the exhaust to the incoming fresh air.
- Run-around coil systems that use a circulating fluid to carry heat from an exhaust coil to an inlet air coil, useful where ducts are far apart.
- Using exhaust heat for other duties such as preheating feed, boiler water or wash water.
Exhaust air from spray dryers carries fine powder, so heat recovery equipment must be designed to resist fouling and be easy to clean. It is usually placed after efficient powder separation. Good separation also improves energy efficiency indirectly, since every kilogram of lost product represents energy wasted; our guide to improving powder recovery in industrial spray dryers covers this in detail.
Tip 5: Choose an Efficient Heating Method
The way the air is heated has a big effect on overall efficiency and cost:
- Direct gas firing passes combustion gases into the drying air, giving high thermal efficiency, but is only suitable where the product can tolerate contact with combustion products.
- Indirect heating through heat exchangers, steam radiators or thermic fluid keeps combustion gases separate, which is essential for many food and pharmaceutical products, at the cost of some exchanger losses.
- Steam radiators are efficient when steam is generated well and condensate is returned to the boiler.
Regardless of the method, regular maintenance matters. Burner tuning, clean heat exchanger surfaces, working steam traps and full condensate return all keep the heater delivering what it should.
Tip 6: Stop Heat Escaping Through Walls and Leaks
Insulation is often damaged during maintenance and never properly repaired. Missing insulation on the chamber, hot air ducts or cyclones wastes energy and can create cold spots where condensation causes deposits. A thermal imaging survey is a quick way to find these spots.
Air leaks have a double cost. In a dryer operating under slight negative pressure, leaks draw in cold ambient air, which lowers the drying temperature and increases the load on the exhaust fan. Common leak points include inspection doors, flange gaskets, rotary valves and expansion joints.
Tip 7: Use Variable Speed Drives and Smart Controls
Fans are among the largest electrical loads in a spray drying plant. Controlling fan speed with variable frequency drives, rather than throttling with dampers, can reduce electrical consumption substantially when the plant runs below full capacity. Automation also helps on the thermal side. Stable outlet temperature control, automatic feed adjustment, burner modulation and variable air volume control prevent the overdrying that wastes energy during unstable operation. AKSH's instrumentation, automation and control systems include PID temperature control, feed pump VFD synchronization and real-time variable air volume and burner modulation designed to optimize fuel, steam and power use.
Tip 8: Improve Operating Practices
Many energy losses come from how the plant is run rather than how it was designed. A simple improvement program often follows these steps:
- Measure specific energy consumption: track fuel or steam used per kilogram of water evaporated, or per kilogram of product.
- Shorten start-up and shutdown: standardize the sequence so the plant reaches stable feed operation quickly.
- Run at steady, near-design capacity: frequent stops and low-load running waste heat in warming and cooling the system.
- Reduce cleaning frequency: addressing wall deposits reduces the number of shutdowns and heat-up cycles.
- Review setpoints regularly: confirm that inlet and outlet temperatures are still appropriate for current products.
- Train operators: help them understand which actions cost energy and which save it.
Tip 9: Consider Inlet Air Conditioning Carefully
Ambient humidity affects drying capacity, particularly during monsoon conditions. Dehumidifying inlet air increases the drying capacity of each kilogram of air and can help with sticky products, but dehumidification itself consumes energy. Whether it saves energy overall depends on the product, the climate and the source of cooling. A heat balance for the specific plant is the best way to decide. In some cases, a seasonal approach works well: running dehumidification only during the most humid months, when capacity losses and stickiness problems are greatest, and bypassing it for the rest of the year.
Tip 10: Keep the Atomizer and Air Disperser in Good Condition
Worn atomizer wheels, eroded nozzle orifices and distorted air disperser vanes do not only affect powder quality. When the spray becomes uneven, operators often compensate by raising the outlet temperature to avoid wet powder and wall deposits, and that extra margin is paid for in fuel. A coarse or uneven spray also needs more residence time to dry fully. Regular inspection of atomizer parts, balancing of rotating components and checks on disperser alignment help keep droplet size consistent, so the plant can run at the lowest outlet temperature the product allows.
Benchmarking Your Plant's Energy Performance
You cannot improve what you do not measure. The most useful single figure is specific energy consumption: the heat supplied by the air heater divided by the water evaporated over the same period. Steam flow meters, gas meters and feed flow and solids data make this calculation possible, and modern control systems can display it continuously. Tracking the figure over weeks shows the effect of each change, reveals gradual deterioration such as fouled heat exchangers or failing insulation, and gives management a clear basis for approving larger investments. Comparing similar products on the same plant, at different times and settings, often highlights the best operating practices worth standardizing.
Prioritizing Your Energy Projects
Not every measure suits every plant. Low-cost operational changes, such as setpoint optimization, insulation repairs and leak sealing, usually come first. Medium-cost projects such as VFDs, control upgrades and feed preheating follow. Larger investments, including evaporator pre-concentration, exhaust heat recovery or conversion to multistage drying, need a proper feasibility study but often deliver the biggest long-term savings. Broader approaches to efficiency across drying operations are discussed in our article on zero-waste drying and reducing energy costs, and food processors will find useful ideas in sustainable spray drying practices for the food industry.
Why AKSH Engineering
AKSH Engineering Systems Pvt. Ltd., based in Ahmedabad, Gujarat, has designed and manufactured spray dryers, evaporators and turnkey drying plants since 2013, with more than 100 installations in India and export markets. Our team of technocrats, with over 100 years of combined experience, approaches energy efficiency as a whole-plant question, combining evaporation, drying, heat recovery and automation where they make sense. Our industrial spray dryers can be engineered with waste heat recovery, multistage configurations and direct or indirect heating options, and our sustainability solutions help plants reduce their wider environmental footprint.
Conclusion
Energy efficiency in spray drying comes from a combination of good design and good operation. Concentrating the feed, optimizing inlet and outlet temperatures, recovering exhaust heat, choosing the right heating method, keeping insulation and seals in good condition, using variable speed drives and smart controls, and running the plant steadily all contribute. Even modest improvements in each area can add up to a significant reduction in fuel and power costs over the life of the plant.
If you would like to assess the energy performance of your existing spray dryer or design a new, more efficient plant, contact the AKSH Engineering team. We will review your heat balance, identify the most promising savings and help you plan upgrades that pay back.