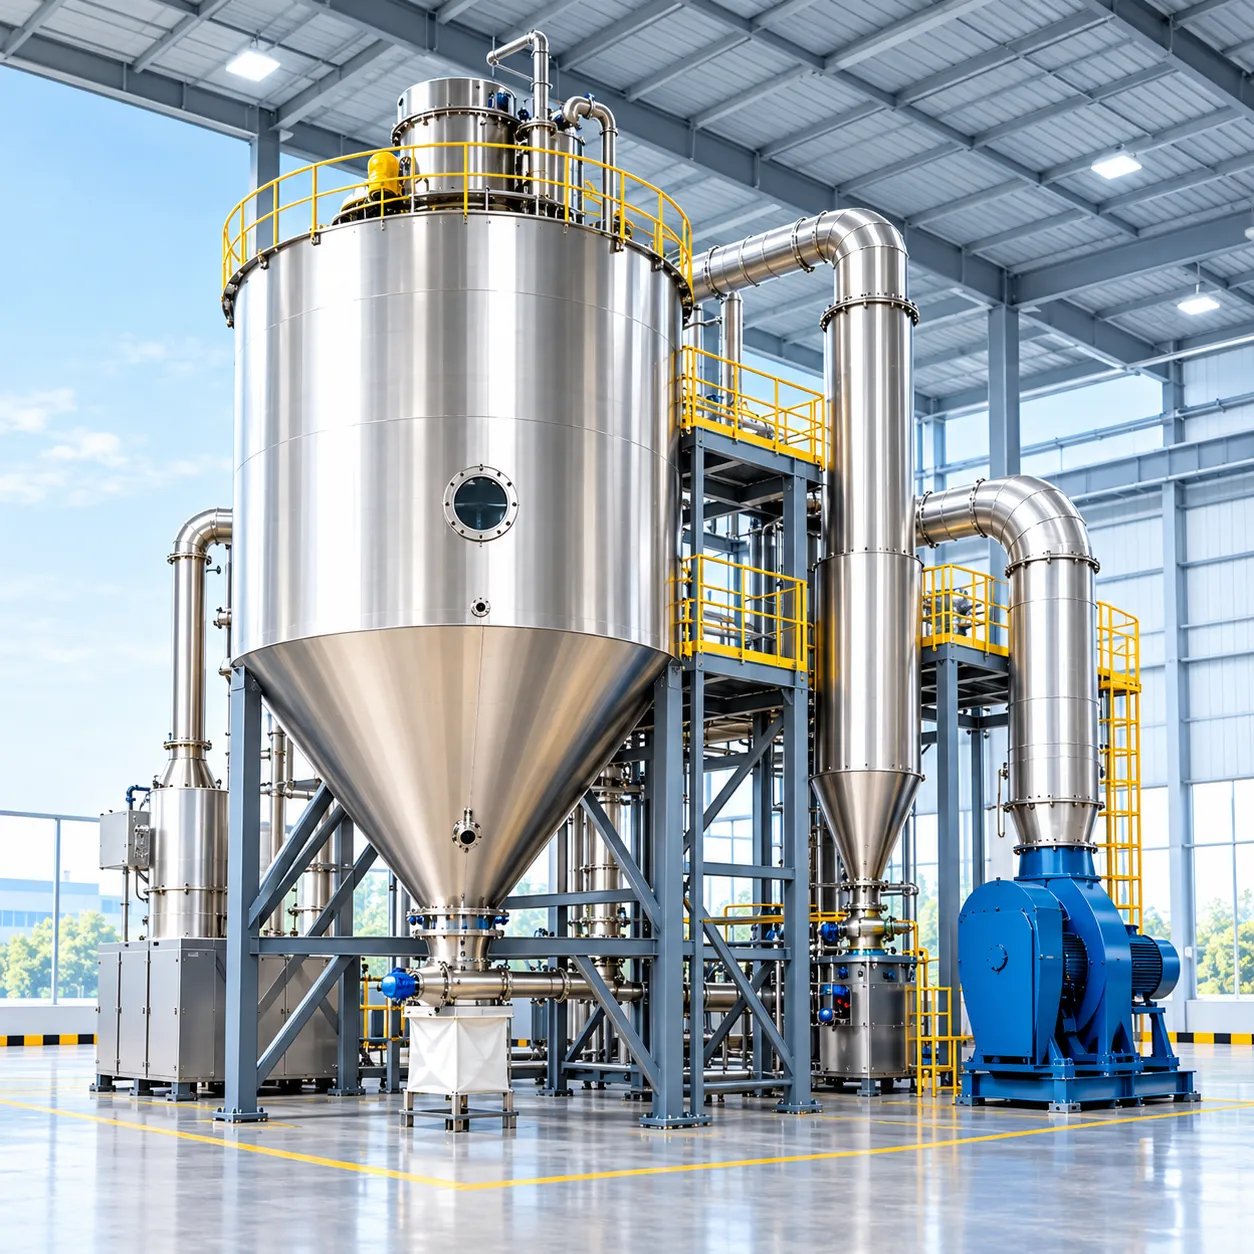

When a company asks for a spray dryer quotation, one of the first questions an engineer sends back is about the powder, not the machine: what particle size, bulk density and flowability does the finished product need, and what does the feed look like before drying? The answers usually decide whether the plant will be built around a high-speed rotary disc atomizer or a set of spray nozzles. Get that choice right and the rest of the design falls into place. Get it wrong and no amount of tuning will produce the powder your customers expect.
This article approaches the rotary-versus-nozzle question from the product side. Rather than a deep dive into nozzle mechanics, which we cover separately in pressure nozzle vs two-fluid nozzle atomization explained, we look at how each atomizer shapes the powder, the tower and the operating budget, and then match common products to the atomizer that usually suits them best.
Two Ways to Make a Spray
A rotary disc atomizer drops the feed onto the center of a wheel spinning at several thousand revolutions per minute. Centrifugal force spreads the liquid into a film across vanes, pins or a smooth disk surface, and the film breaks into droplets as it is flung from the rim. The spray travels outward horizontally in an umbrella shape.
A nozzle atomizer creates the spray by forcing liquid through a small orifice, either at high pressure (single-fluid pressure nozzle) or with the help of compressed air or gas (two-fluid nozzle). The spray leaves as a cone, usually pointing down the axis of the tower.
Both reach the same goal of creating a huge droplet surface area for rapid drying, but they produce different droplet populations and demand different chambers. AKSH Engineering builds both: rotary disk atomization systems with VFD-controlled speeds of about 5,000 to 25,000+ RPM, and nozzle atomization systems in pressure and two-fluid configurations.
Start with the Powder You Want
The most reliable way to choose an atomizer is to work backward from the powder specification. Four properties do most of the deciding.
Particle Size
Rotary atomizers typically produce a fine to medium powder, and particle size is easy to adjust because droplet size falls as wheel speed rises. Pressure nozzles generally produce coarser particles; on AKSH nozzle spray dryers, nozzle-produced powders typically fall in the range of about 80 to 250 microns. If your product must be coarse enough to flow freely and avoid dusting without a separate agglomeration step, the nozzle often has the edge. If you need a fine, uniform powder or the ability to move quickly between grades, the wheel is usually more convenient.
Bulk Density
Nozzle sprays tend to form denser, more compact particles. Rotary wheels, particularly vaned wheels, can draw air into the liquid film and produce particles with more internal voids, which lowers bulk density. For products sold by weight in fixed-volume packs, such as detergent or some dairy powders, this difference can matter commercially.
Particle Shape and Flow
Pressure nozzles are well known for spherical, free-flowing beads, which is why they are popular for detergents, ceramic granules for pressing and other products that must fill dies or containers evenly. Rotary powders are also largely spherical, but finer particles flow less easily and may need agglomeration or a fluid bed stage to improve handling.
Particle Size Distribution
Both atomizers can deliver a reasonably narrow distribution when they are operated well. Rotary wheels hold their distribution steady across a wide range of feed rates, while a pressure nozzle performs best close to its design point. If production rates will swing widely, that stability is a real advantage for the wheel.
Then Look Hard at the Feed
The powder target tells you what you want; the feed tells you what is possible.
- Abrasive slurries: mineral, ceramic and pigment slurries erode small orifices quickly. A rotary wheel has no fine orifice in the atomizing zone, and wear can be managed with hard-faced or carbide inserts on the wheel. Abrasive feeds are therefore a classic rotary application, as discussed in our article on spray drying ceramic pigments and frit.
- High solids and suspended particles: crystals, fibers and lumps can block nozzle passages, while the open rim of a rotary wheel tolerates them well.
- High viscosity: rotary wheels handle a broad viscosity range without needing extreme pump pressures. Pressure nozzles need ever-higher pressure as viscosity rises, while two-fluid nozzles can cope but at the cost of more compressed gas.
- Clean, low-viscosity solutions: both options work, so other factors such as particle size, plant height and energy decide.
- Solvent-based feeds: both can be used in closed-loop nitrogen systems; the decision is usually driven by particle size and capacity rather than the solvent itself.
How the Atomizer Shapes the Plant
Atomizer choice is never just a component decision, because the spray pattern dictates the geometry of the drying chamber.
Chamber Diameter and Height
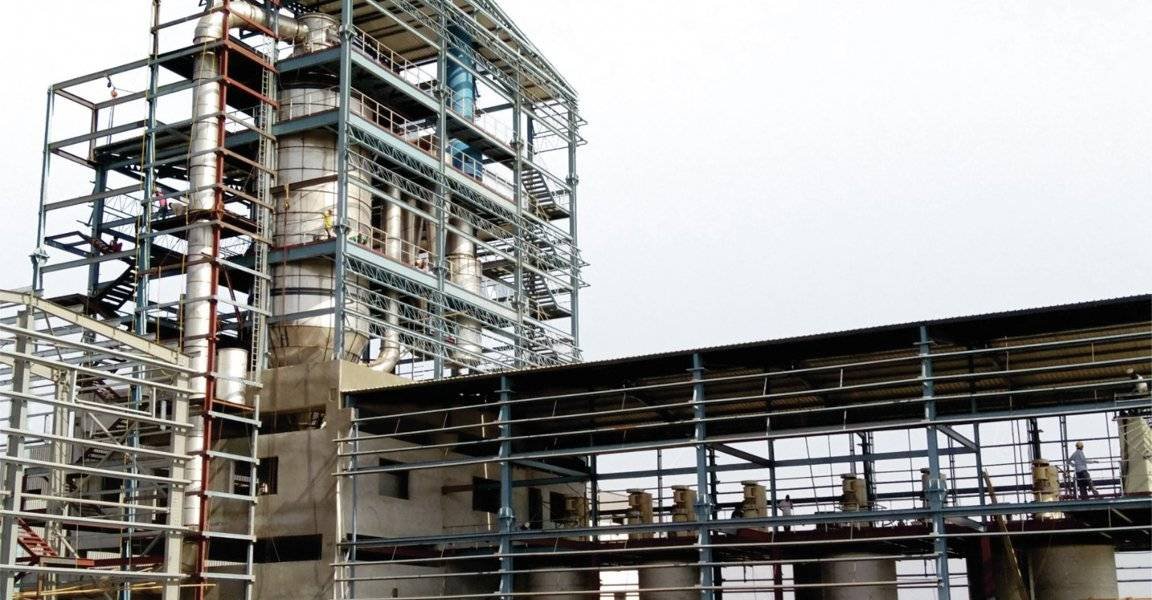
A rotary wheel throws droplets outward, so the chamber must be wide enough for droplets to dry before they reach the wall. Rotary towers are therefore relatively large in diameter with a moderate cylinder height. A pressure nozzle sprays downward in a narrow cone, and its coarser droplets need a longer fall to dry, so nozzle towers are typically tall and slender. This affects building height, structural steel, platforms and the footprint you must reserve on site.
Capacity and Scaling
A single rotary atomizer can handle very large feed rates; AKSH rotary systems are built for capacities from about 100 LPH to 50,000+ LPH, custom sized. Nozzle plants scale by adding more nozzles, each on its own lance, which keeps the droplet size consistent but adds pumps, piping and lances to maintain.
Turndown
Rotary wheels can be run at reduced feed rates while maintaining droplet size by adjusting speed, which helps plants that operate at different loads. Pressure nozzles have a narrower comfortable operating range; reducing throughput substantially often means switching off lances or changing nozzle inserts.
Side-by-Side: Rotary Disc vs Nozzle
| Factor | Rotary Disc Atomizer | Nozzle Atomizer |
|---|---|---|
| Spray direction | Horizontal umbrella from the wheel rim | Downward (or upward fountain) cone |
| Typical powder | Fine to medium, adjustable by wheel speed | Medium to coarse, dense, free-flowing |
| Bulk density | Lower to medium | Medium to higher |
| Abrasive or high-solids feeds | Well suited with wear-resistant wheels | Orifice wear and clogging risk |
| Viscous feeds | Broad viscosity range | Needs high pressure or atomizing gas |
| Chamber shape | Wider diameter, moderate height | Taller, narrower tower |
| Turndown | Good; adjust feed and speed | Narrower; add or remove lances |
| Main maintenance | Wheel inspection, balancing, bearings, drive | Nozzle inserts, orifices, high-pressure pump |
| Typical products | Milk, coffee, dyes, pigments, ceramics, effluents | Detergents, granules, coarse food powders |
Product-by-Product Guide
Every formulation is different, so treat the following as typical starting points rather than rules. Real trials should confirm the choice.
Dairy and Food Powders
Milk powders, whey, coffee and tea extracts, maltodextrin and fruit powders are commonly dried on rotary atomizers, which handle concentrated feeds smoothly and give flexible control of particle size. Some dairy and instant-food producers use pressure nozzles when they want coarser, denser particles, often combined with a fluid bed for agglomeration. For a wider look at food applications, see spray drying in the food industry.
Detergents
Detergent powders are a textbook nozzle application. The tall-tower, pressure-nozzle arrangement produces hollow, spherical, free-flowing beads with controlled bulk density.
Ceramics, Minerals and Pigments
Abrasive slurries favor rotary wheels with hard inserts for long service life. Where a coarse, dense, pressable granule is required, as with some ceramic tile bodies, pressure nozzles in a fountain arrangement are also used. The right answer depends on the granule specification and how much wear the plant can tolerate.
Dyes and Agrochemicals
Dye solutions and many agrochemical formulations are often dried on rotary atomizers because they combine high throughput with tolerance for varying solids content and viscosity.
Pharmaceuticals and Nutraceuticals
Fine APIs, encapsulated actives and herbal extracts are frequently dried with two-fluid nozzles at small and medium scale, and with rotary atomizers at larger scale. Hygienic design, cleanability and recovery of fine particles often matter as much as the atomizer itself.
Effluents and ZLD Streams
High-TDS effluents contain dissolved and suspended salts that can crystallize and block nozzles. Rotary atomizers are the usual choice for drying these streams to a solid salt in zero liquid discharge plants.
Maintenance and Operating Cost
The two technologies spend their maintenance budgets in different places. A rotary atomizer is a precision high-speed machine: the wheel must stay dynamically balanced, bearings and lubrication must be monitored, and vibration should be checked routinely. Wheel inserts wear on abrasive duty and are replaced as a set. A pressure nozzle system concentrates its wear in small, inexpensive parts, the orifice discs and swirl inserts, but it also relies on a high-pressure pump whose seals and valves need attention. Two-fluid nozzles add the cost of compressed air or nitrogen.
In energy terms, pressure nozzles are efficient per kilogram of feed, rotary atomizers consume moderate motor power, and two-fluid nozzles become expensive at very large scale due to compressed-gas demand. Capital cost is project-specific: the rotary atomizer itself is a sophisticated unit, while a nozzle tower may require more building height. Comparing complete plant designs, not just atomizer prices, gives the true picture.
A Simple Decision Path
- Write down the powder specification: particle size range, bulk density, flowability, moisture and dust limits.
- Characterize the feed: solids content, viscosity, abrasiveness, presence of crystals or fibers, and any solvents.
- Fix the throughput and its variation: steady high capacity, or frequent changes between products and loads?
- Check site constraints: available building height, floor area and utilities such as compressed air.
- Shortlist the atomizer: coarse, dense, free-flowing powder from a clean feed points toward nozzles; abrasive, viscous or variable feeds and fine powders point toward a rotary wheel.
- Prove it with a trial: run the real feed on a pilot unit with the shortlisted atomizer and measure the powder.
The last step is where most uncertainty disappears. A pilot spray dryer with interchangeable rotary and two-fluid atomization lets you test both routes on the same feed, and our article on how pilot spray dryers help achieve consistent particle size explains how those trials are structured.
Common Mistakes When Choosing an Atomizer
- Copying a competitor's plant: two companies making the "same" product may have very different feeds and powder specifications. What works for one may not suit the other.
- Choosing on atomizer price alone: the atomizer is a small part of total plant cost, but it decides chamber size, building height and long-term maintenance.
- Ignoring future products: if the plant may later run different grades or formulations, the flexibility of a rotary wheel or interchangeable atomization can be worth more than a perfect fit for today's product.
- Assuming lab results transfer directly: small laboratory dryers almost always use two-fluid nozzles, so their particle size says little about how the feed will behave on a production wheel or pressure nozzle.
- Underestimating feed variability: seasonal raw materials or upstream process changes can shift solids content and viscosity, which a pressure nozzle tolerates less easily than a rotary wheel.
Why AKSH Engineering
AKSH Engineering Systems Pvt. Ltd. has designed and manufactured spray drying plants in Ahmedabad, Gujarat, since 2013, with more than 100 installations delivered. Our technocrats, with over 100 years of combined experience, engineer both atomization routes in-house, so our recommendation is based on your product rather than on the one technology we happen to sell. Our rotary systems use dynamically balanced wheels in smooth, vane, pin and serrated-rim designs, with SS316L, duplex steel, Hastelloy and tungsten carbide options for demanding feeds. Our nozzle systems cover pressure and two-fluid designs with carbide and ceramic wear parts. Both are integrated into complete industrial spray dryers, and the full range is listed under atomization technologies.
Conclusion
Rotary disc atomizers and nozzle atomizers are both proven, but they are suited to different products. The rotary wheel shines with abrasive, viscous or variable feeds, high capacities and fine powders with flexible size control. The nozzle excels when the product calls for coarse, dense, free-flowing particles from a clean, stable feed. Start from the powder specification, respect the realities of the feed, and confirm the choice with a trial before you commit to a full-scale design.
If you are weighing up atomization options for a new product or an expansion, contact the AKSH Engineering team. Tell us about your feed and your powder targets, and we will help you choose the atomizer and dryer configuration that suits your product.